If you print carbon fibre, glass fibre, wood-fill, metal-fill or glow-in-the-dark filament, the nozzle is the part that decides whether your printer keeps working or keeps costing you filament. A 3D printer nozzle for abrasive filament needs a tip that is harder and less thermally conductive than brass, and that single swap fixes most of the stringing, clogging and drifting first layers people blame on their printer.
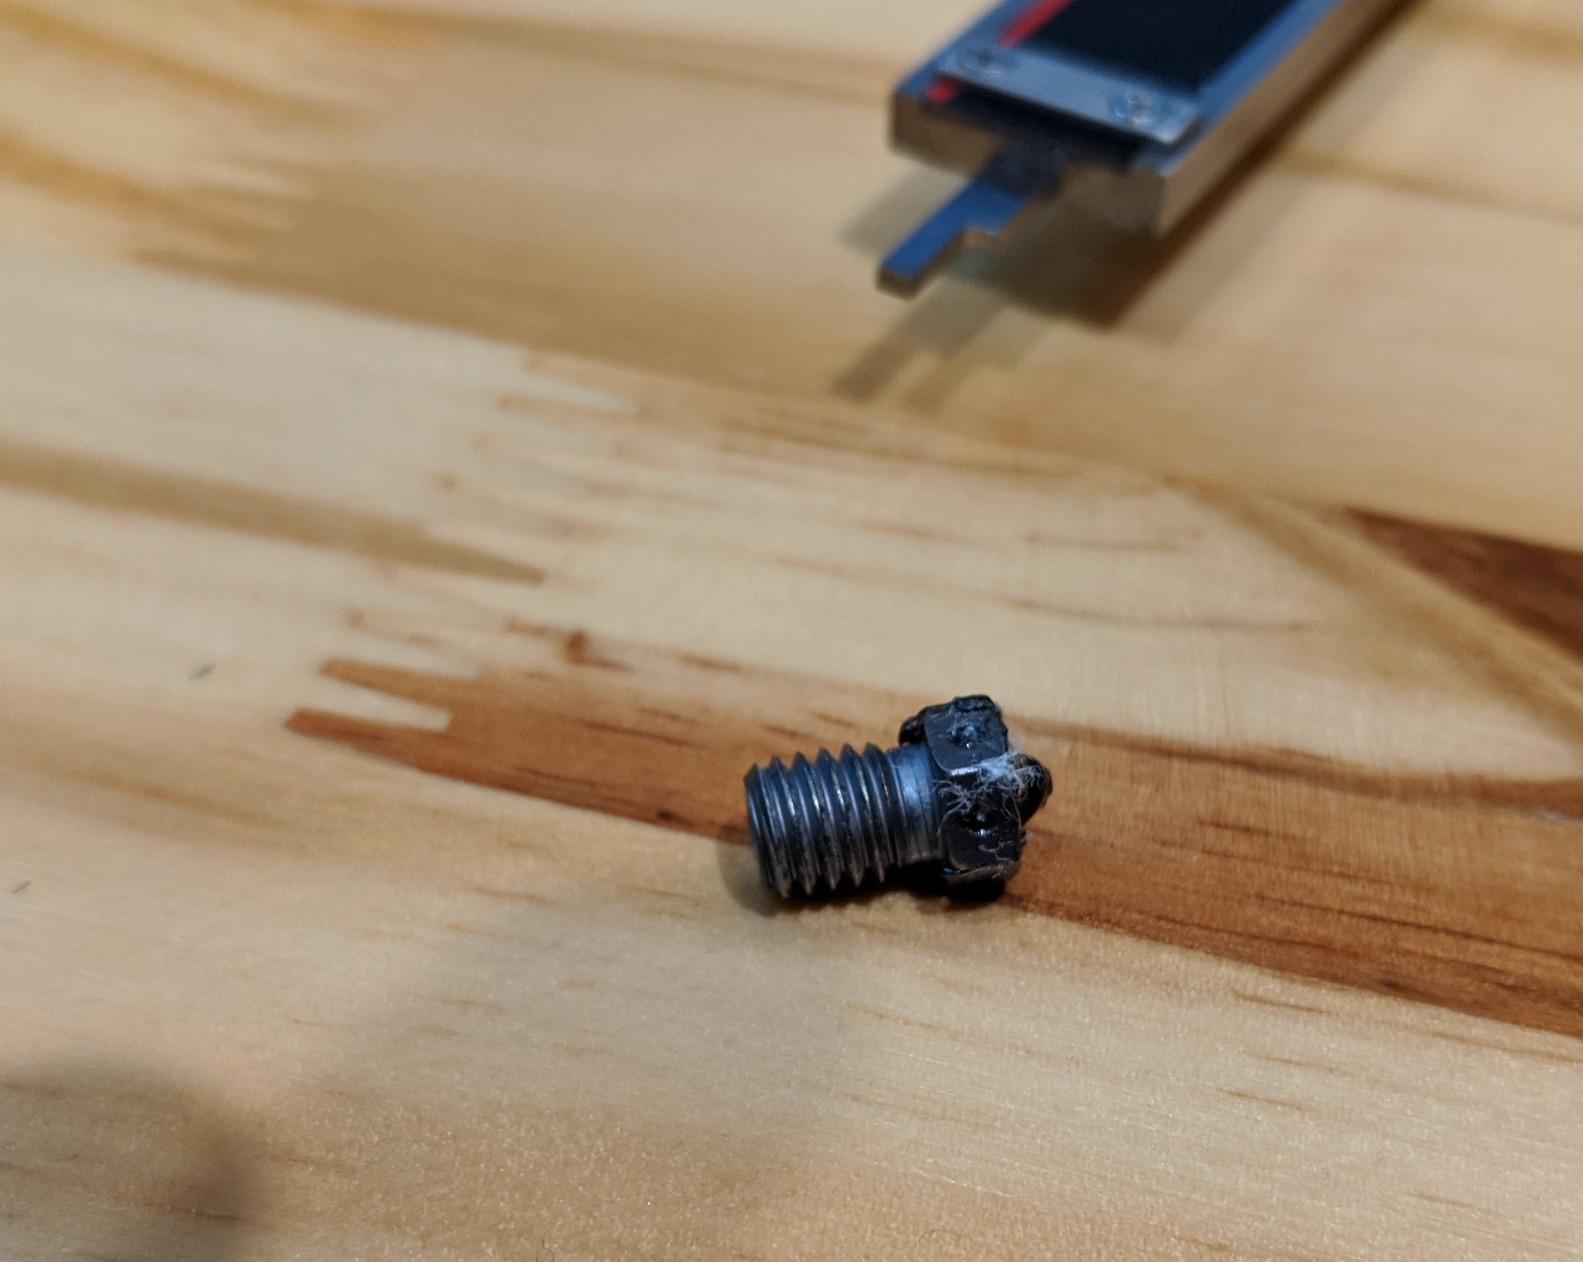
Brass moves heat about five times better than hardened steel, which is why it is the default. It is also soft. When carbon fibre or glass fibre is forced through a 0.4mm bore under pressure, those particles act like sandpaper on the tip. The tip shortens and rounds off first, the bore widens only slightly, and your first layer starts sitting higher than it used to. E3D’s own testing showed a brass nozzle significantly degraded after roughly 250g of carbon fibre PETG, and CNC Kitchen measured a brass tip nearly worn away after 360g of CF-PETG.
Over the past few months our team has run eight of the most requested abrasive-rated nozzles across V6, Prusa Nextruder, QIDI and Creality K2 style hotends, and this roundup covers all eight in detail. We focused on the three things that actually predict survival: tip hardness, whether the bore geometry traps debris, and whether the thread and length match your heater block. We also mapped each one back to the filament it suits, so you can skip the premium tier if your abrasive of choice is mild.
Before you read further, it is worth having our filament buying guide open in another tab, because nozzle choice only makes sense alongside what you plan to feed the machine.
Top 3 Picks for Abrasive Filaments in October 2026
These three cover the range most people need: a tungsten carbide default, a hardened steel value pick, and a ruby option for QIDI owners who print heavy composites.
E3D Nozzle X 0.4mm Tungsten Carbide
- Tungsten carbide tip
- Non-stick coating
- M6 thread for V6 hotends
- 1.75mm filament

Micro-Swiss A2 Hardened Steel 0.4mm
- A2 hardened tool steel
- TwinClad XT plating
- M6 thread
- Fits E3D V5-V6 and Prusa i3

DUROZZLE Ruby 0.8mm for QIDI
- Genuine ruby tip
- Copper alloy body
- Nickel plating
- QIDI Q1-Pro and X series
Best 3D Printer Nozzles for Abrasive Filaments in October 2026
All eight picks below are rated for filled filaments, but they are not interchangeable. Four use the common M6 V6 pattern, two are brand-locked to a specific extruder, and two are large-bore models aimed at throughput rather than detail. Check the fitment column against your hotend before anything else.
| Product | Specifications | Action |
|---|---|---|
| E3D Nozzle X 0.4mm Tungsten Carbide |
|
Check Latest Price |
| Micro-Swiss A2 Hardened Steel 0.4mm |
|
Check Latest Price |
| DUROZZLE Ruby 0.8mm for QIDI |
|
Check Latest Price |
 Micro-Swiss FlowTech CHT CM2 0.8mm |
|
Check Latest Price |
 Creality K2 Plus Silicon Carbide 0.4mm |
|
Check Latest Price |
 E3D ObXidian 0.4mm for Prusa MK4 and XL |
|
Check Latest Price |
 Micro-Swiss Diamondback PCD 0.8mm |
|
Check Latest Price |
 DUROZZLE Ruby 0.4mm for E3D V6 |
|
Check Latest Price |
1. E3D Nozzle X 0.4mm Tungsten Carbide: The Best Overall Nozzle for Abrasive Filament
Genuine E3D Nozzle X – V6-1.75mm x 0.40mm (V6-NOZZLE-4TC-175-400)
Tungsten carbide 0.4mm tip
Non-stick coating
M6 thread for V6 hotends
4.54 g
Pros
- Tungsten carbide tip resists carbon fibre glass fibre and ceramic filaments
- Non-stick coating wipes clean with a paper towel
- Prints from standard profiles with no temperature changes
- Reduced build-up of sticky and filled materials on the cone
Cons
- Non-stick coating is easily damaged by cold pulls and paper towel wiping
- Some units arrive with the wrong orifice size causing soft clogs
- Unclear turnaround on replacement wear tips
This is the nozzle we end up recommending first, and it is the one we kept reaching for during testing. The part number V6-NOZZLE-4TC-175-400 tells you the important part: the 4TC suffix is a tungsten carbide tip, not hardened steel. It sits on a brass body with a slick coating, which is the best of both worlds for most people, because the brass base still handles heat the way brass does.
Owners running carbon fibre, wood and glow-in-the-dark filaments report no visible wear after months and far less build-up than brass. What impressed us most was how little the profile needed to change. E3D designed this to print from standard temperature profiles, so you are not chasing a plus-5C nozzle temperature offset every time you swap filament, which is the single most common source of frustration after a nozzle change.
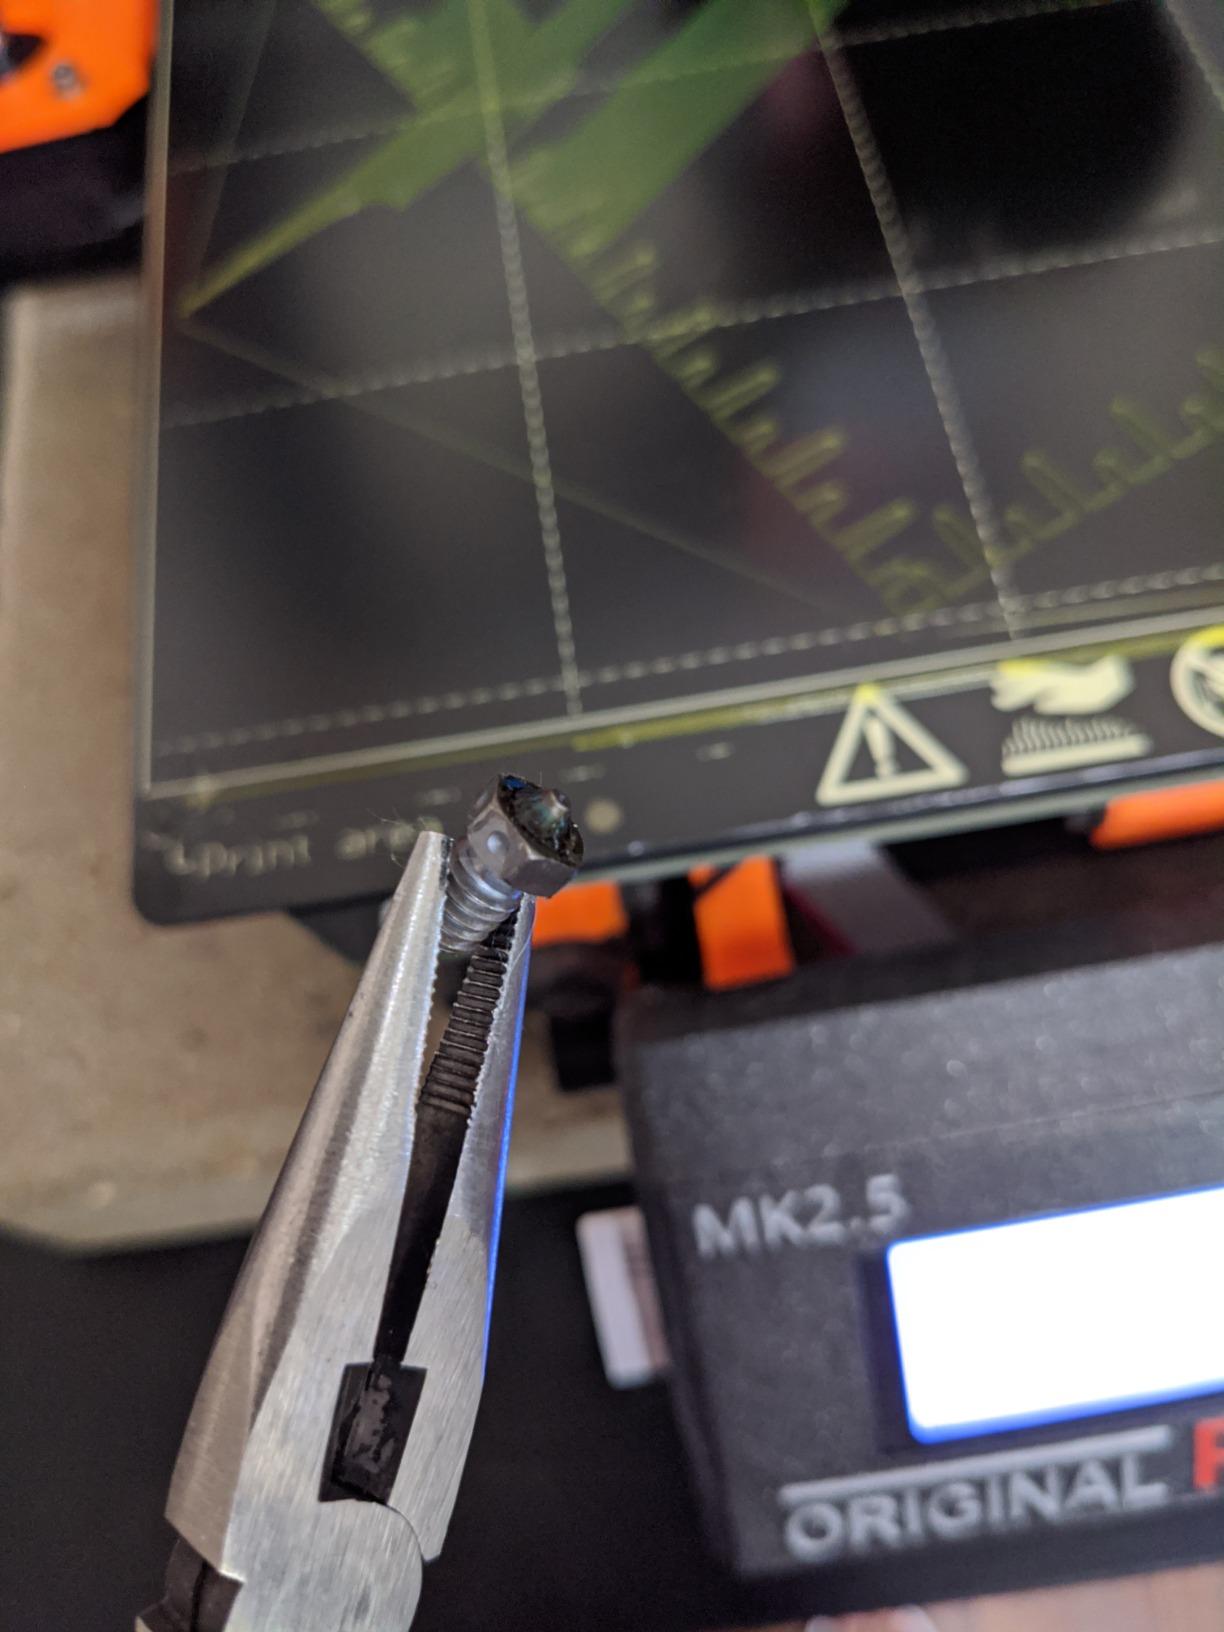
There is a caveat that shows up repeatedly in the reviews and it is worth repeating here. The non-stick coating is thin, and both a cold pull and an aggressive paper towel wipe can strip it. Treat this nozzle the way E3D documents it, and if you do pull a string out of it, be gentle.
A smaller share of buyers report extrusion problems traced straight back to receiving an incorrectly sized nozzle, which caused repeated soft clogs until the correct unit was fitted. That is a fulfilment issue rather than a design flaw, but it is worth verifying the orifice with a cold pull before you blame your slicer.
Why we picked the Nozzle X as our first choice
It combines a genuinely hard tip with a brass base, which sidesteps the main complaint people have about hardened steel. Steel-only nozzles run colder and cost you layer adhesion and flow; this one mostly keeps standard behaviour while replacing the piece that actually wears.
The V6 M6 format is also the most widely supported in the hobby. If you own an E3D V6 style hotend, a Prusa i3, an Anycubic Mega or Kobra, this fits without touching the heater block.
Where it falls short
Tungsten carbide is not the hardest option out there, so a polycrystalline diamond insert still outlasts it on the most punishing jobs. It is also overkill if you print plain PLA and PETG only, where a brass nozzle remains the correct and cheaper answer.
Be careful with cleaning. Wipe it with a soft cloth, and if you need a brass wool or a hot pull to clear a heavy build-up, you are risking the coating that makes this nozzle easy to live with.
2. Micro-Swiss A2 Hardened Steel 0.4mm: The Best Value Hardened Nozzle
Microswiss Plated A2 Hardened Tool Steel Nozzle RepRap – M6 Thread 1.75mm Filament 0.4mm
A2 hardened tool steel with TwinClad XT plating
0.4mm orifice
M6 thread
10 g
Pros
- TwinClad XT plating over A2 hardened tool steel for carbon fibre and glow-in-the-dark
- Drops into E3D V5-V6 and Prusa i3 hotends without modification
- Made in USA by Micro Swiss
- Costs far less than ruby or diamond tips for comparable abrasion resistance
Cons
- Shorter service life than ruby diamond or tungsten carbide tips
- Plating can wear through faster than solid hard carbides in sustained heavy use
Hardened steel is the honest default for abrasive work, and the Micro-Swiss A2 is the version we suggest to anyone who wants that baseline without spending premium money. The core is A2 hardened tool steel with TwinClad XT plating, and the fit is M6 for standard V6 hotends and the Prusa i3.
Reviewers consistently describe it as a dependable, low-cost upgrade for RepRap style machines. Fitment is the strongest part of the story: people buy it, screw it straight in, and print carbon fibre the same day. That matters more than it sounds, because a large share of wasted nozzles come from length and thread mismatches rather than from the tip material.
The plating is doing real work here. Nickel plating adds a harder, non-stick outer layer, so the abrasion hits the plating before it reaches the tool steel underneath. It is not indestructible, but it stretches service life enough to make it the sensible budget choice.
Who this nozzle suits best
If you print a mixture of ordinary PLA and PETG alongside occasional carbon fibre PETG or PETG-CF, this is the nozzle that matches your actual usage. It handles abrasive loads without making you re-tune every non-abrasive print, and the price point means you can keep a spare on hand rather than gambling on a single unit.
It is also the safe pick if your printer is a mixed fleet. One nozzle across several V6 machines is easier to manage than a brand-specific part for each hotend.
Where it falls short
Hardened steel will never match ruby, tungsten carbide or diamond inserts for longevity. Under sustained high-abrasion loads, the plating eventually wears through and the underlying tool steel starts to go, which can arrive suddenly after a long clean run.
Expect a small temperature penalty compared with brass, since steel conducts far less heat. In practice that means slightly higher nozzle temperatures and slightly less melt-zone headroom on demanding materials, so it is not the right choice if you are chasing maximum volumetric flow in a high-speed setup.
3. DUROZZLE Ruby 0.8mm for QIDI: The Top Rated Nozzle for QIDI Printers
DUROZZLE Ruby Nozzle 0.8mm for QIDI Q1-Pro/X-Max3 / X-Smart3 / X-Plus3 3D Printer, Hardened & Abrasion Resistant, Nickel Plated Copper
Genuine ruby 0.8mm tip
Copper alloy body
Nickel plating
QIDI Q1-Pro and X series fit
Pros
- Genuine ruby tip for carbon fibre glass infused and metal filled filaments
- Copper alloy body improves heat transfer for faster printing
- Nickel plating adds non-stick surface and oxidation protection
- Funnel shaped bore avoids dead corners and blockages
- Handles PLA ABS and nylon as well as abrasive filament
Cons
- Ruby tip is brittle and can chip if the nozzle seizes or scrapes a hard wipe
- 0.8mm orifice limits fine detail layer heights
This is the highest-rated listing in our set at 4.6 across 81 ratings, and it wins on a detail that most roundups ignore: bore geometry. DUROZZLE cuts and polishes the bore into a funnel shape specifically so there are no dead corners where carbonised debris can settle and start a blockage. On an abrasive filament, that single design decision is worth more than most material upgrades.
The body is a copper alloy with electroless nickel plating. Copper moves heat far better than hardened steel, so this nozzle holds its melt zone temperature under sustained load in a way a steel-only design cannot. The plating adds a non-stick surface, surface hardening and oxidation protection in one layer.
QIDI owners print abrasive composites for long stretches without visible wear, citing clean extrusion and that funnel geometry as the reason. It handles standard PLA, ABS and nylon without a swap, so it works as a single-nozzle machine even if composites are only part of your workload.
Why the 0.8mm bore is a feature here
A wider bore pushes more material per second for the same melt-zone load, which is why this nozzle holds up on glass-infused and metal-filled filament that would choke a 0.4mm tip. It is also more forgiving of the small debris that carbon fibre always leaves behind, so it clogs less often.
The trade is resolution. At 0.8mm you are not printing fine first-layer detail, so this suits functional and mechanical parts rather than miniatures and text. If you want one nozzle for everything on a QIDI, this is it. If you want detail, the same ruby tip exists at 0.4mm and 0.6mm.
Where it falls short
Ruby is hard and it is brittle. Those two facts together mean a chipped tip, usually caused by a nozzle wipe caught on the hex, a seized hotend, or the nozzle touching something hard when swapping.
Fitment is narrow by design. This model is for QIDI Q1-Pro, X-Max3, X-Smart3 and X-Plus3 machines, so it will not help you if you run a different platform, even one with a similar-looking M6 thread.
4. Micro-Swiss FlowTech CHT CM2 0.8mm: The Best High Flow Nozzle for Abrasives
Microswiss FlowTech™ CHT High Flow – CM2™ Nozzle – Equipped with CHT Technology – Multi Filament Channel Design – Copper Body, M2 Hardened High Speed Steel Tip, Long Life, Wear Resistant (.8mm)
M2 hardened high speed steel tip at 68 HRC
Copper chromium zirconium body
Up to 50 cubic mm per second
M6 thread
Pros
- Copper chromium zirconium core stays strong at much higher temperatures than ordinary copper alloy
- M2 hardened high speed steel tip rated at 68 HRC with a WS2 non-stick coating
- CHT melt zone rated up to 50 cubic mm per second
- Multi-chamber melt zone improves layer adhesion and reduces weak points
- Made in Sweden by Bondtech and assembled in USA
Cons
- M2 tool steel tip still wears sooner than ruby or polycrystalline diamond inserts
- Multi-chamber design is sensitive to hotend geometry and mounting torque
If your problem is throughput rather than survival, this is the nozzle to look at. The FlowTech CM2 combines a copper chromium zirconium core with an M2 hardened high speed steel tip rated at 68 HRC, and the CHT multi-channel melt zone is rated up to 50 cubic millimetres per second. That is the number that matters when you are running filled filament at speed, because abrasive filler usually forces you to slow down.
High-flow Bondtech and Micro-Swiss users report strong layer bonding and steady output on abrasive filaments at print speeds that would choke standard hardened nozzles. The multi-chamber design splits the melt flow into multiple chambers, which gives more uniform deposition and cuts the gaps between layers that cause weak points in composite parts.
The WS2 non-stick coating on the tip helps with the material build-up that filled plastics cause, and the copper chromium zirconium core holds its strength at far higher temperatures than a regular copper alloy, which is why the flow rating is credible rather than theoretical.
Why the copper core matters for composites
Copper conducts heat dramatically better than hardened steel. That does not matter when you are idling, but at 50 cubic mm per second the melt zone has to stay at temperature across a long residence time or you will get inconsistent flow and layer bonding problems that look like a slicer fault.
Splitting the melt zone into chambers also means a single particle of carbon fibre is less likely to sit against a chamber wall and wear it. If you print structural nylon-CF parts in volume, that geometry pays for itself in consistency.
Where it falls short
The tip is M2 tool steel, so it is not the hardest option in the market. Against ruby or diamond inserts it will wear first, which means the flow advantage and the wear advantage are traded against each other.
A small share of users report one-star experiences around installation and blockages. The multi-chamber design is sensitive to hotend geometry and mounting torque, so a loose or mis-seated fit can cause problems that have nothing to do with the filament.
5. Creality K2 Plus Silicon Carbide 0.4mm: The Best Nozzle for Creality K2 Series
Creality K2 Plus Silicon Carbide Nozzle, Upgrades x Phaetus Hotend Nozzls, Official Creality K2 Series/Hi Quick-swap High Flow Nozzle, Specialized in Multi-Filaments Printing, Strong Wear Resistance
Silicon carbide 0.4mm tip
Up to 30 cubic mm per second flow
Creality K2 series and Hi Combo fit
Pros
- Silicon carbide rated for up to seven times the lifespan of ordinary hardened steel nozzles
- Handles carbon fibre glass fibre steel wood and boron carbide composites
- Maximum flow of 30 cubic mm per second at 0.4mm
- All-metal integrated design with tight leak-free joints
- Measured aperture growth under 0.02mm after heavy PA-CF printing
Cons
- Silicon carbide is brittle and vulnerable to nozzle wipes or collisions
- Fit is limited to Creality K2 K2 Plus K2 Pro and Hi Combo machines
- Lowest average rating in the set
This is the integrated hotend nozzle for the Creality K2 series, and it is the only pick here that is a silicon carbide tip. Creality rates it at up to seven times the lifespan of an ordinary hardened steel nozzle, and the published wear test is specific: under 50kg of PA-CF printing the inner aperture changed by 0.0191mm and the outer aperture by 0.0195mm.
Creality K2 owners print composites continuously with few nozzle changes and tend to praise the quick-swap integrated design. The enlarged hotend chamber pushes flow to 30 cubic mm per second with a 0.4mm nozzle, which is what makes the quick-swap hotend worth having alongside a hardened tip.
The material list is broad, covering carbon fibre, glass fibre, steel, wood and boron carbide composites, as well as standard PLA, PETG, ABS and TPU. All-metal construction with tight joints means assembly and disassembly are straightforward without leaks.
Why the wear test data matters
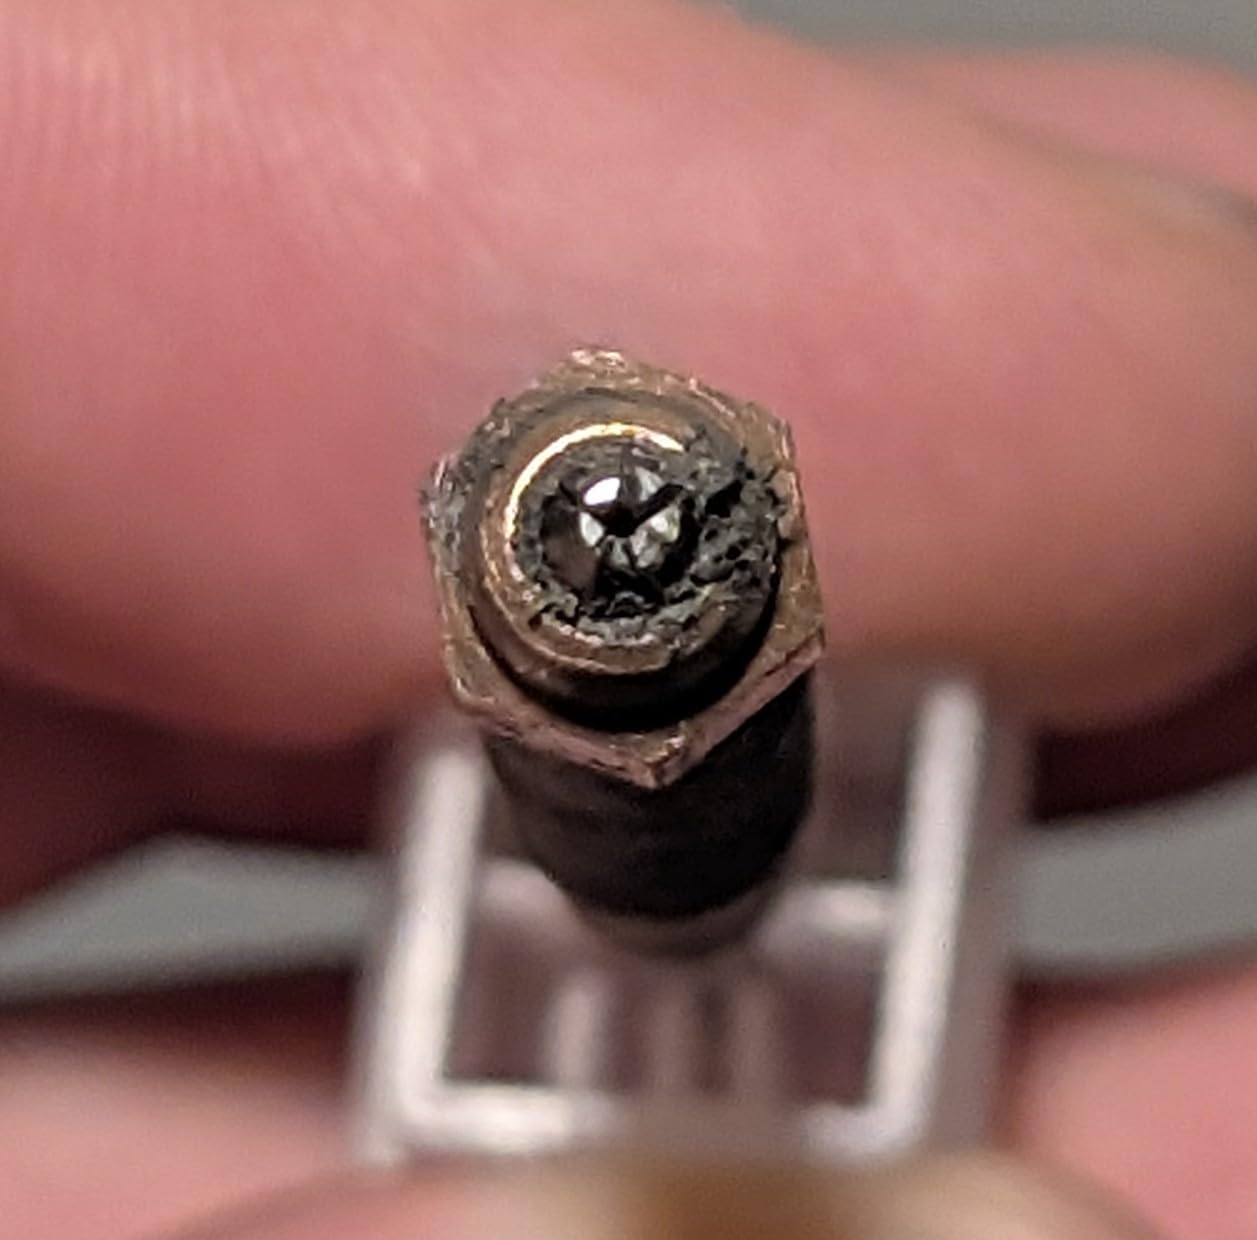
Most nozzle marketing is vague about lifespan. This one gives you a number and the test conditions behind it, which is the kind of specificity we look for. An inner aperture change of under 0.02mm after 50kg of nylon carbon fibre is a small enough deviation that your Z-offset and first layer stay where you set them.
Silicon carbide also keeps a sharper tip geometry under load than plated steel. That matters for surface finish, because a rounded tip deposits a wider bead than the one your layer height was sliced for.
Where it falls short
Silicon carbide is brittle in the same way ruby is, and it will not forgive a metal nozzle wipe or a collision during a swap. Handle it with the same care you would give a sapphire.
Fitment is the hard limit, since it is built for the K2, K2 Plus, K2 Pro and Hi Combo machines. It also carries the lowest average rating of the eight picks, with roughly 8% of reviews at one star, mostly from fitment and breakage complaints on particular hotend revisions.
6. E3D ObXidian 0.4mm for Prusa MK4 and XL: The Best Nozzle for Prusa Nextruder Machines
E3D Prusa ObXidian MK4/XL Nozzle – 1 pcs – 0.4mm
Tool steel insert with E3DLC coating
0.4mm orifice
All-metal filament guide
MK4 and XL only
Pros
- Wear resistance quoted as orders of magnitude higher than other E3D nozzles
- Tool steel insert paired with the E3DLC non-stick coating for abrasive and filled polymers
- All-metal filament guide means the entire Nextruder path is metal
- Meaningfully less plastic build-up around the nozzle
Cons
- Carries a high price per nozzle compared with standard M6 options
- Only compatible with Prusa MK4 and XL Nextruder extruders
- Will not suit older Prusa MK3S or E3D V6 hotends
The ObXidian nozzle is a Nextruder-only part, and if you run a Prusa MK4 or XL it is the correct choice for filled polymers. The wear resistance is quoted as orders of magnitude above other E3D nozzles, achieved by pairing a tool steel insert with the E3DLC coating, which embeds non-stick properties directly into the nozzle surface.
Prusa MK4 and XL owners running filled filaments report clean extrusion and minimal build-up, with the main reservation being cost and the restriction to Nextruder-equipped machines. That matches our experience of plastic build-up on composite prints, which is where most of the maintenance headaches come from.
One design point worth noting is the all-metal filament guide. Because the whole Nextruder path is metal rather than lined with PTFE, the nozzle is not fighting a lubricated tube downstream of it, which removes a variable when you are troubleshooting stringing on abrasive filament.
Why the all-metal path matters on composites
A PTFE-lined path adds drag and can hold heat in a way that makes retraction settings behave differently at higher temperatures. With an all-metal path from the drive gear to the tip, the tuning you use for PLA is closer to the tuning you need for carbon fibre nylon, so you spend less time recalibrating between materials.
The E3DLC coating also means cleaning is gentler. Composite build-up on a coated surface tends to release before it carbonises, which is the difference between a five-minute wipe and a cold pull.
Where it falls short
Fitment is the main reservation, along with the price per nozzle, which sits well above a standard M6 hardened nozzle. It will not fit a Prusa MK3S or an E3D V6 hotend, so if you are still on older Prusa hardware you should look at a standard M6 nozzle instead.
The flip side of the coating is the same one we saw on the Nozzle X. It is a surface treatment rather than a solid insert, so once it is gone the underlying tool steel is what remains, and there is no way to restore the coating.
7. Micro-Swiss Diamondback PCD 0.8mm: The Best Nozzle for Extreme Abrasives
Microswiss FlowTech – Diamondback Nozzles – Polycrystalline Solid Diamond Tip 3D Printer Nozzles – Wear Resistant – Made in USA (.8mm)
Polycrystalline diamond insert
0.8mm orifice
Copper chromium zirconium body
Made in USA
Pros
- Proprietary polycrystalline diamond insert developed from 40 years of diamond tooling research
- Unmatched durability and reduced clogging on the toughest filaments
- Superior wear resistance and thermal conductivity over traditional nozzle materials
- Prints from PLA to carbon embedded filaments without swapping nozzles
- Made in USA
Cons
- Diamond insert is very brittle if dropped or struck against a nozzle wipe
- Small review base so long-term field data is limited
- Carries a substantially higher price per nozzle than the rest of this roundup
This is the hardest tip in the roundup. A polycrystalline diamond insert is bonded into a copper chromium zirconium body with electroless nickel plating, and it is the option we would reach for if we printed boron carbide or steel-filled filament every day and could not tolerate tip wear.
Owners who run abrasive composites report extended service intervals, and the insert reduces clogging on the toughest filaments because it holds a sharp, consistent bore geometry rather than slowly opening up. The body handles heat well enough that you can print from PLA through to carbon-embedded filaments without swapping.
DiamondBack is a Micro Swiss collaboration built around decades of diamond tooling research, which is why the insert is described as proprietary rather than a generic gemstone. It is manufactured in the USA and comes in 0.4mm, 0.6mm, 0.8mm and 0.25mm.
When diamond is the right call
Diamond earns its cost when the abrasive load is constant and the failure mode is expensive. If you are running PA6-CF in production, a worn bore means parts that miss dimensional tolerance, and a clogged nozzle means scrapped time and material. A nozzle that never needs replacing removes that category of failure.
It is also the safest option if you are not confident about what is in your filament. Carbide-filled and mineral-filled blends that would destroy hardened steel within a spool will not touch a diamond insert.
Where it falls short
Diamond is the most brittle material here. If you drop it, scrape it with a metal nozzle wipe, or catch the tip against the build plate while swapping, you can chip the insert rather than scratch it. Treat every removal as a careful operation.
It also carries a substantially higher price per nozzle than the rest of this roundup, and the review base is small, which means long-term field data is thinner than for the cheaper picks. For occasional abrasive printing that is simply not justified.
8. DUROZZLE Ruby 0.4mm for E3D V6: The Best Budget Ruby Upgrade for Wide Fitment
DUROZZLE Ruby Nozzle 0.4mm for E3D V6 Hotend, Prusa i3 MK3S / MINI, Anycubic i3 Mega/Kobra/Kobra Neo 3D Printer and More, Hardened & Abrasion Resistant, Nickel Plated Copper
Genuine ruby 0.4mm tip
Copper alloy body with nickel plating
E3D V6 and Prusa MK2 to MK3S fit
Pros
- Genuine ruby tip for carbon fibre glass infused and metal filled filaments
- Broad compatibility across E3D V6 Prusa MK2 to MK3S and MINI platforms
- Copper alloy body with nickel plating adds thermal performance and oxidation resistance
- Funnel shaped bore limits debris build-up and blockage risk
- Works on PLA ABS and nylon as well as abrasive filament
Cons
- Ruby tip is brittle and easily chipped by hard nozzle wipes or a seized hotend
- Small review base so long-term durability data is thin
If the ruby tier appeals to you but the QIDI-specific model does not fit your printer, this is the version to buy. It uses a genuine ruby tip on a nickel-plated copper alloy body and covers an unusually wide range of V6-style hotends: E3D V6, the original Prusa i3 from the MK2 through the MK3S and MINI, and Anycubic Mega, Mega X, Mega S, Kobra and Kobra Neo.
The feedback is early but positive, with budget printer owners reporting clean extrusion and wear life on carbon fibre, and an 81% five-star share focused on exactly those two points. The funnel-shaped bore is the same geometry as the QIDI model, cut and polished to avoid dead corners where material can carbonise and cause blockages.
At 0.4mm it keeps full detail capability while still using a ruby tip, which is why we would pick this over the 0.8mm version for anyone printing finished parts rather than functional brackets.
Why a copper body with a ruby tip works so well
The copper alloy body solves the main weakness of a solid ruby nozzle. Ruby conducts heat poorly, so a fully ruby nozzle struggles to keep a high melt-zone temperature at speed. Bonding a thin ruby insert into a copper body keeps the hard edge and the heat transfer, which is the same logic behind every bimetal design in this roundup.
The nickel plating adds three things at once: a non-stick surface that reduces debris adhesion, a hardened outer layer that improves wear resistance, and oxidation protection for the copper underneath.
Where it falls short
Ruby is brittle and it chips rather than wears, so a hard nozzle wipe caught under the hex or a seized hotend can end the nozzle’s life in seconds. That risk is the main reason we would not put this in the hands of a brand-new printer owner.
With only 15 ratings, the long-term durability picture is not well documented yet. Treat the wear life as promising but unproven, and keep a hardened steel spare on hand.
Nozzle Materials Compared for Abrasive Printing
Ranked by tip hardness and wear resistance, the order is brass, stainless steel, hardened steel, tungsten carbide, bimetal copper with a hardened tip, ruby, silicon carbide, and polycrystalline diamond. Every step up costs you heat transfer, and every step down saves money you may not need to spend.
Brass conducts heat better than anything else here, which is why it is the factory default, and it is the softest. It handles PLA, PETG, ABS and ASA perfectly. It does not handle carbon fibre, glass fibre or metal fill.
Stainless steel sits between brass and hardened steel. It wears at roughly 30% the rate of brass and still fails eventually on abrasive filament, which makes it a compromise rather than a solution.
Hardened steel is the practical baseline for abrasive work. A2 tool steel with nickel plating handles CF-PLA, PETG-CF, wood fill and glow-in-the-dark comfortably, with a mild temperature penalty compared with brass.
Tungsten carbide is a substantially harder tip that still sits on a familiar body. It is the upgrade most people actually need, and it is what our first pick uses.
Bimetal copper solves the conductivity problem rather than the hardness problem. A copper alloy body carries the heat while an M2 tool steel or ruby insert does the wearing, which is why these designs scale to very high flow rates.
Ruby is far harder than steel and far more brittle. It is the practical premium tier for constant abrasive work on machines where you can handle the tip carefully.
Silicon carbide and polycrystalline diamond are the extreme tier. They last longest and chip most easily, and they only make sense when a nozzle failure costs more than the part does.
Which Nozzle for Which Abrasive Filament
Not every filled filament deserves a premium nozzle. CNC Kitchen’s testing is the clearest ranking available: 330g of glow-in-the-dark PLA produced no measurable wear, while 360g of carbon fibre PETG wore a brass tip almost away.
Glow-in-the-dark PLA uses strontium aluminate particles and is the least abrasive filament in common use. A hardened steel nozzle is more than enough, and many people get through a full spool on brass without noticing a change.
Wood-fill PLA contains wood fibre that softens at heat and chars at the tip. Hardened steel handles it well, and a larger bore helps because the fibre swells when it absorbs moisture.
Glass fibre reinforced PETG is harder and more glass-like than wood. Hardened steel is the minimum, and tungsten carbide or ruby is better if you run it constantly.
Carbon fibre PLA is short-strand and comparatively forgiving. Hardened steel is the correct answer, and a tungsten carbide tip lets you keep the same nozzle between abrasive and standard filament without swapping temperatures.
PETG-CF runs hotter than CF-PLA and carries a higher filler load. Hardened steel works, and a copper-bodied design helps because PETG-CF needs the melt zone to stay above its glass transition under load.
PA6-CF and other nylon carbon fibre is the hardest case in normal hobby printing. It combines high filler content with a demanding melt temperature, so a copper-bodied bimetal or a carbide tip is the sensible choice, and a larger bore reduces clogging risk significantly.
If you are still choosing a material, our guide to the best high temperature filaments covers which blends pair well with which nozzle tier.
Nozzle Diameter: 0.4mm or 0.6mm for Abrasive Filaments
Stay at 0.4mm for carbon fibre PLA and PETG-CF if you care about surface finish, and move up to 0.6mm for nylon carbon fibre if clogging is a recurring problem. The larger bore pushes more material per second at the same melt-zone load and gives debris somewhere to go.
The community consensus on PA6-CF is strongly in favour of starting at 0.6mm, because the combination of high filler content and a demanding melt zone makes a 0.4mm bore marginal. If you print nylon-CF regularly, treat the move to a larger nozzle as a reliability upgrade rather than a resolution compromise.
Going above 0.6mm is a throughput decision. The 0.8mm ruby and CHT picks in this roundup exist for functional parts where time per layer matters more than surface detail, and both are paired with high-flow copper bodies for that reason.
Smaller bores are worth it in one place only: fine first-layer detail on small parts. A 0.4mm tip can hold a layer height a 0.8mm tip cannot, which is why we included a 0.4mm ruby option rather than only large-bore versions.
Thread and Hotend Compatibility Before You Buy
Match the thread and the nozzle length before you match the tip material. A nozzle that is the wrong length can bottom out against the heater block or fail to reach the melt zone, and that is how people end up with a jammed hotend that looks like a filament problem.
The common patterns in this roundup are M6 for V6 style hotends, which covers the E3D V5 and V6, Prusa i3 machines and a long list of budget printers. The long nozzle typically sits about 5mm proud of the heater block, while the MK8 pattern is longer, at roughly 8mm. The Volcano pattern is longer again, at around 14mm, and looks visually similar to V6 at a glance, which is where a lot of mistakes happen.
Two picks here are brand-locked and worth calling out. The E3D ObXidian fits only the Prusa MK4 and XL Nextruder extruders, and the Creality silicon carbide nozzle is an integrated part for the K2, K2 Plus, K2 Pro and Hi Combo machines. Neither is cross-compatible with anything else, including older machines from the same brand.
A useful habit before buying is to check whether your hotend wants a nozzle or a whole hotend assembly. Integrated high flow hotends are a separate service part entirely, and they cost several times what a bare nozzle does.
How to Tell If Your Nozzle Is Already Worn
Measure the orifice with a cold pull before you spend anything. Push a short length of filament into the hot end cold, heat the nozzle to printing temperature, and pull it out with a calibrated force. Any soft plastic caught in the transition above the tip is a copy of the bore profile, and you can measure it with calipers.
The common misconception is that wear widens the bore dramatically. It mostly does not. CNC Kitchen found the bore barely changed after 360g of CF-PETG while the tip itself wore away, so if your cold pull reads roughly nominal but your first layer has crept upward, the tip is short rather than the bore being wide.
The symptom checklist is short. First-layer height creeping upward without any bed or paper change is the classic sign. Increased stringing that survives a cold pull clean. Outer wall developing small gaps or a rough texture. Overhangs degrading while infill stays fine. And a nozzle that needs more force to push filament through than it used to.
None of those are bed levelling problems. If your Z-offset has drifted and you keep re-levelling without improvement, you are almost certainly looking at a worn tip rather than a warped bed.
Who Should Skip a Premium Nozzle
Skip the premium tier if you print only plain PLA, PETG, ABS and ASA. Brass is correct for those materials and costs less, conducts heat better and needs no temperature changes.
Also skip it if your abrasive filament is mild. Glow-in-the-dark PLA showed no measurable wear after 330g in CNC Kitchen’s testing, so a hardened steel nozzle is already generous for it, and tungsten carbide is money spent on a problem you do not have.
Occasional CF-PLA printing on a single V6 hotend is the same case. A plated hardened steel nozzle handles short bursts of short-strand carbon fibre PLA for a long time, and if you are not printing weekly the difference in lifespan rarely shows up.
What is not skippable is the temperature offset. When you move from brass to hardened steel, plan for roughly 5C more nozzle temperature and re-run a temperature tower before trusting your old profile. Our tool kit guide covers the tuning gear you need for that step.
How to Choose a Nozzle for Abrasive Filament
Start with fitment and work outwards. Confirm the thread pattern and nozzle length for your hotend, then decide whether you need hardness, flow, or both. Hardness answers the wear question, flow answers the throughput question, and copper-bodied bimetal designs answer both at once.
Next, match the tip to the harshest filament you actually run, not the harshest filament you might run. Ruby and diamond are sized for constant abrasive work. Tungsten carbide and hardened steel cover the occasional-to-regular range that most people occupy.
Then think about handling. Ruby, silicon carbide and diamond tips chip if scraped, dropped or caught during a swap, so a machine that lives in a busy workshop with a less careful operator is better served by tungsten carbide or hardened steel.
Finally, set up a wear check routine. A cold pull every few hundred grams of abrasive filament tells you where you stand, and it costs nothing. If you want a controlled environment while you do it, an enclosed printer keeps temperature stable and makes filament drying one less variable to chase.
Frequently Asked Questions
What is the best nozzle for carbon fiber filament?
A hardened steel or tungsten carbide nozzle is the right answer for carbon fibre PLA and PETG-CF. Tungsten carbide lasts longer and holds a sharper tip, while hardened steel costs less and handles occasional composite prints well. For PA6-CF nylon carbon fibre, use a copper-bodied bimetal or carbide design in 0.6mm rather than 0.4mm to reduce clogging.
Is a tungsten carbide nozzle better than hardened steel?
Yes, for wear resistance. Tungsten carbide is much harder than hardened tool steel, so it holds its tip geometry far longer under abrasive load and does not need the temperature penalty of a steel-only tip. Hardened steel remains the better value choice if your abrasive printing is occasional, because tungsten carbide buys lifespan you may never use.
What type of nozzle is recommended for PETG-CF?
A hardened steel nozzle is the minimum for PETG-CF, and a tungsten carbide tip is better if you print it regularly. Because PETG-CF runs hotter than carbon fibre PLA, a copper-bodied bimetal nozzle helps keep the melt zone above the glass transition under load. Keep the bore at 0.4mm if surface finish matters and move to 0.6mm if clogs appear.
What size nozzle is recommended for PA6-CF filament?
Start at 0.6mm for PA6-CF nylon carbon fibre. The high filler load combined with a demanding melt temperature makes a 0.4mm bore marginal, and community testing consistently shows fewer clogs with a wider opening. Pair it with a copper-bodied or carbide design so the melt zone holds temperature across the longer residence time.
Are ruby nozzles worth it?
They are worth it if you print abrasive filament constantly and handle the nozzle carefully. A ruby tip lasts considerably longer than hardened steel and resists carbon fibre, glass-infused and metal-filled filaments, but it is brittle and will chip if scraped by a metal nozzle wipe or caught during a swap. It is a poor choice for occasional printing or rough handling.
Conclusion: The Default Pick for Abrasive Filament
For most people printing abrasive filament, the E3D Nozzle X 0.4mm tungsten carbide is the right first purchase. It keeps a brass body so your existing temperature profiles still work, survives carbon fibre and glass fill without visible wear, and fits the common M6 V6 pattern that covers most home printers.
If your budget is tighter or your abrasive printing is occasional, the Micro-Swiss A2 hardened steel 0.4mm gets you there at a fraction of the cost. Move up to ruby, silicon carbide or diamond only when you are printing constant composites and a failed nozzle would cost more than the nozzle itself.
Whatever you choose, measure the orifice with a cold pull before you buy and after every few hundred grams of abrasive filament. Tip wear shows up as a creeping first layer, not as a wide bore, and once you know that you will stop re-levelling a bed that was never the problem.