The strongest carbon fiber filaments for strong parts are the ones built on an engineering polymer, not the ones with the biggest carbon fiber number on the label. Our top pick, the OVERTURE PLA Matte CF, is the easiest place to start, while load-bearing work calls for a nylon or polycarbonate base such as the IEMAI PA6-CF or the PRILINE PC-CF. Carbon fiber adds stiffness and dimensional stability. It does not add impact toughness, and the base polymer decides how much load a part can actually carry.
That distinction is where most buying guides go wrong. They rank spools by marketing language and leave you to find out that a reinforced PLA bracket snapped under a load that a cheap PETG-CF part would have survived. So we built this roundup around one question: which spool produces a part that holds shape, heat and load, and what does it take to print it.
We compared 10 carbon fiber filaments across PLA, PETG, polycarbonate and nylon bases, weighing published fiber content, heat deflection and tensile data, layer adhesion, warping behaviour, and the hardware each one demands before it will print reliably. Every pick below lists its stated fiber percentage, its nozzle and enclosure requirements, and the honest weakness that shows up in reviews. Updated for 2026.
Two things come up constantly in printing communities, on r/3Dprinting and the Bambu Lab forum alike, and both matter more than the spool you choose. The first is moisture: nylon-based carbon fiber that has not been dried will bubble, string and clog no matter which brand it is. The second is orientation: a carbon fiber part printed on its weakest axis will delaminate long before the filament itself gives up. We cover both in the buying guide below.
Top 3 Carbon Fiber Filaments for Strong Parts in October 2026
Three spools cover most strong-part jobs, whether you are printing drone frames, tooling or camera mounts. The first is the easiest to print, the second is the strongest bulk option, and the third handles heat better than anything else here.

OVERTURE PLA Matte CF 1.75mm
- Matte PLA base
- Carbon fiber reinforced
- Dimensional accuracy +/- 0.02 mm
- 1kg spool

IEMAI PA6-CF 3kg Spool
- 20% chopped carbon fiber
- PA6 nylon base
- Heat resistance to 150C
- 3kg spool
PRILINE Carbon Fiber PC 1.75mm
- Polycarbonate blend
- Chopped carbon fiber
- Prints at 255-280C
- 1kg spool
All 10 Picks Compared Side by Side in October 2026
Every spool in this roundup appears below with the numbers that decide whether it belongs in your printer. Fiber content is stated by weight, the base polymer sets the ceiling on strength, and the difficulty column tells you whether your machine is ready for it.
| Product | Specifications | Action |
|---|---|---|
| OVERTURE PLA Matte Carbon Fiber Filament 1.75mm 1kg |
|
Check Latest Price |
| IEMAI PA6-CF Carbon Fiber Nylon Filament 1.75mm 3kg |
|
Check Latest Price |
| PRILINE Carbon Fiber Polycarbonate Filament 1.75mm 1kg |
|
Check Latest Price |
 SainSmart ePA-CF Carbon Fiber Filled Nylon 1.75mm 1kg |
|
Check Latest Price |
 TINMORRY PETG-CF Carbon Fiber PETG Filament 1.75mm 1kg |
|
Check Latest Price |
 SUNLU PA6-CF20 Carbon Fiber Nylon Filament 1.75mm 1kg |
|
Check Latest Price |
 Polymaker Fiberon PA612-CF15 Carbon Fiber Nylon 1.75mm 0.5kg |
|
Check Latest Price |
 Polymaker Carbon Fiber PLA Filament Black 1.75mm 1kg |
|
Check Latest Price |
 ELEGOO PETG-CF 3D Printer Filament 1.75mm Black 1KG |
|
Check Latest Price |
 SUNLU PA12-CF 20% Carbon Fiber Nylon Filament 1.75mm 1KG |
|
Check Latest Price |
1. OVERTURE PLA Matte Carbon Fiber Filament 1.75mm 1kg
OVERTURE PLA Matte Carbon Fiber Filament 1.75mm, 1kg Carbon Fiber Black
Matte PLA base
1.75mm 1kg spool
Dimensional accuracy +/- 0.02 mm
Pros
- Noticeably stiffer than basic PLA
- Smooth clog-free extrusion once dialled in
- Matte finish hides layer lines
- Tight winding resists tangling
Cons
- Spool is not vacuum sealed
- Needs drying before printing
- Cardboard spool can arrive bent
This is the spool we hand to anyone whose carbon fiber filament for strong parts ambitions start with cosmetic hardware, camera cages, brackets and housings. The carbon fiber reinforcement raises stiffness well above basic PLA, and the matte surface does an unusually good job of hiding the layer lines that normally give reinforced PLA away. At 6,824 reviews it is also the most thoroughly tested filament in this roundup by a wide margin.
Printing it needs almost nothing special. A standard desktop printer running around 210C on the nozzle handles it, and the reported experience is clean extrusion with very little stringing once the first layer is set. If you are moving up from standard PLA, our PLA filament beginner guide covers the baseline settings this sits on top of.
The catch is the drying. The spool is not vacuum sealed, so treat it like any other open PLA and run it through a dryer first. Reviewers also flag temperature sensitivity: prints come out inconsistent at 200C on some machines and behave properly closer to 210C. Small parts can struggle with bed adhesion, so a brim or a glue stick helps more than raising bed temperature.
Dimensional accuracy is quoted at +/- 0.02 mm using an optical measuring system, and the winding is tight enough that tangling is rare. That combination matters if you are printing mating parts that need to slot together, which is the situation where reinforced PLA earns its keep. It is not the situation where you need heat resistance, and we would not put it under a hot engine bay or in a sunlit car.
Who this filament suits
It suits anyone with a normal printer who wants a part that resists bending and cracking far better than plain PLA while still printing at low temperature with no enclosure. The matte black finish means it doubles as a visible part, so it works for camera rigs, desk hardware, model detailing and enclosures as well as for structural bits.
It is also an easy entry into reinforced filament, which matters if this is your first time switching a spool. There is no drying marathon and no 290C nozzle to worry about before you know whether you like the material.
Where it falls short
Reinforced PLA is stiffer and more brittle than plain PLA, so a thin cantilevered arm can snap instead of flexing. If your part needs to absorb an impact, take a look at the PETG-CF options further down instead. And if the part lives above 60C, this is the wrong spool entirely.
Cardboard spool quality is the other recurring complaint. It is a cosmetic issue for most people, but if you plan to run a dry box or an AMS-style unit, budget for a proper spool or an adapter.
2. IEMAI PA6-CF Carbon Fiber Nylon Filament 1.75mm 3kg
IEMAI PA6-CF Carbon Fiber Nylon Filament 1.75mm, Matte Black, 3kg Spool
PA6 base with 20% chopped carbon fiber
3kg spool
Heat resistance up to 150C
Pros
- High stiffness and load-bearing stability
- Wear resistant for gears and bushings
- Reduces warping and shrinkage
- Matte surface hides layer lines
Cons
- Best results need an enclosed chamber
- Abrasive fiber needs a hardened nozzle
- 3kg spool is bulky to handle
This is the bulk pick, and the one we would buy if we were printing strong parts all week. Twenty percent chopped carbon fiber in a PA6 nylon base gives you a genuine engineering thermoplastic: high stiffness, low friction, and heat resistance up to 150C according to the manufacturer. Gears, bushings, sliding assemblies and heat-exposed mounts are the jobs it was built for.
The 3kg format is the real differentiator. If you are running out of filament mid-project on a functional part, the changeover stop is a genuine waste of time, and a large spool of reinforced nylon is the material most likely to run out. Handling is the trade-off, because a 3kg spool is a two-handed operation on most racks.
Layer adhesion is the headline strength claim here, and reviewers consistently describe strong interlayer bonding with reduced warping and shrinkage compared with unfilled nylon. That combination matters more than raw tensile numbers for a printed part, because most failures in FDM happen between layers rather than inside them.
Accuracy is quoted at +/- 0.03 mm, and the matte industrial finish reduces visible layer lines enough that parts do not need heavy post-processing. Just plan for the hardware: a closed chamber is listed as the condition for best results, and the abrasive fiber demands a hardened steel nozzle.
Who this filament suits
It suits anyone with an enclosed printer and a hardened nozzle who prints mechanical parts in volume and wants nylon-level strength with far less warping than plain PA6. If your work involves sliding contact, gears or sustained heat, the wear and low-friction characteristics are the reason to choose it over a PLA-based alternative.
For a single small bracket, a 1kg spool makes more sense. For a production run of fixtures or brackets, this is the pick that keeps the material cost and downtime down.
Where it falls short
PA6 is a moisture magnet, and a 3kg spool that is opened repeatedly will absorb water faster than a sealed 1kg roll. Drying is not optional with this material, and skipping it produces the bubbling and stringing that community members complain about most often.
The surface finish is matte and slightly textured, so if appearance matters more than load, a nylon or ASA filament will look better. We covered more of the temperature picture in our high temperature filament guide.
3. PRILINE Carbon Fiber Polycarbonate Filament 1.75mm 1kg
PRILINE Carbon Fiber Filament, PRILINE Carbon Fiber Polycarbonate 3D Printer Filament 1.75mm, High Strength Carbon Fiber 3D Printing Filament 1kg Spool, Black
Chopped carbon fiber in a polycarbonate blend
1.75mm 1kg spool
Prints at 255-280C
Pros
- Rigid parts that can be drilled and tapped
- Exceptionally low warping
- Matte black finish hides layer lines
- Low odor during printing
Cons
- Cooling fan must be off for adhesion
- Some buyers call it a PC/PLA alloy
- Eats brass nozzles quickly
Polycarbonate is the base polymer to reach for when heat is the constraint, and this is the only PC-based spool in the group. Reviewers report parts that are hard enough to be drilled and tapped without the threads stripping, which is exactly what you need from a tool handle, jig or fixture. The carbon fiber fill keeps warping far lower than you would expect from a PC blend.
It also prints more easily than the reputation of PC suggests, though not without conditions. The hot end runs 255-280C on a 90-100C bed, and the cooling fan has to stay off or layer adhesion suffers badly. That single setting is the difference between a usable part and a delaminated one.
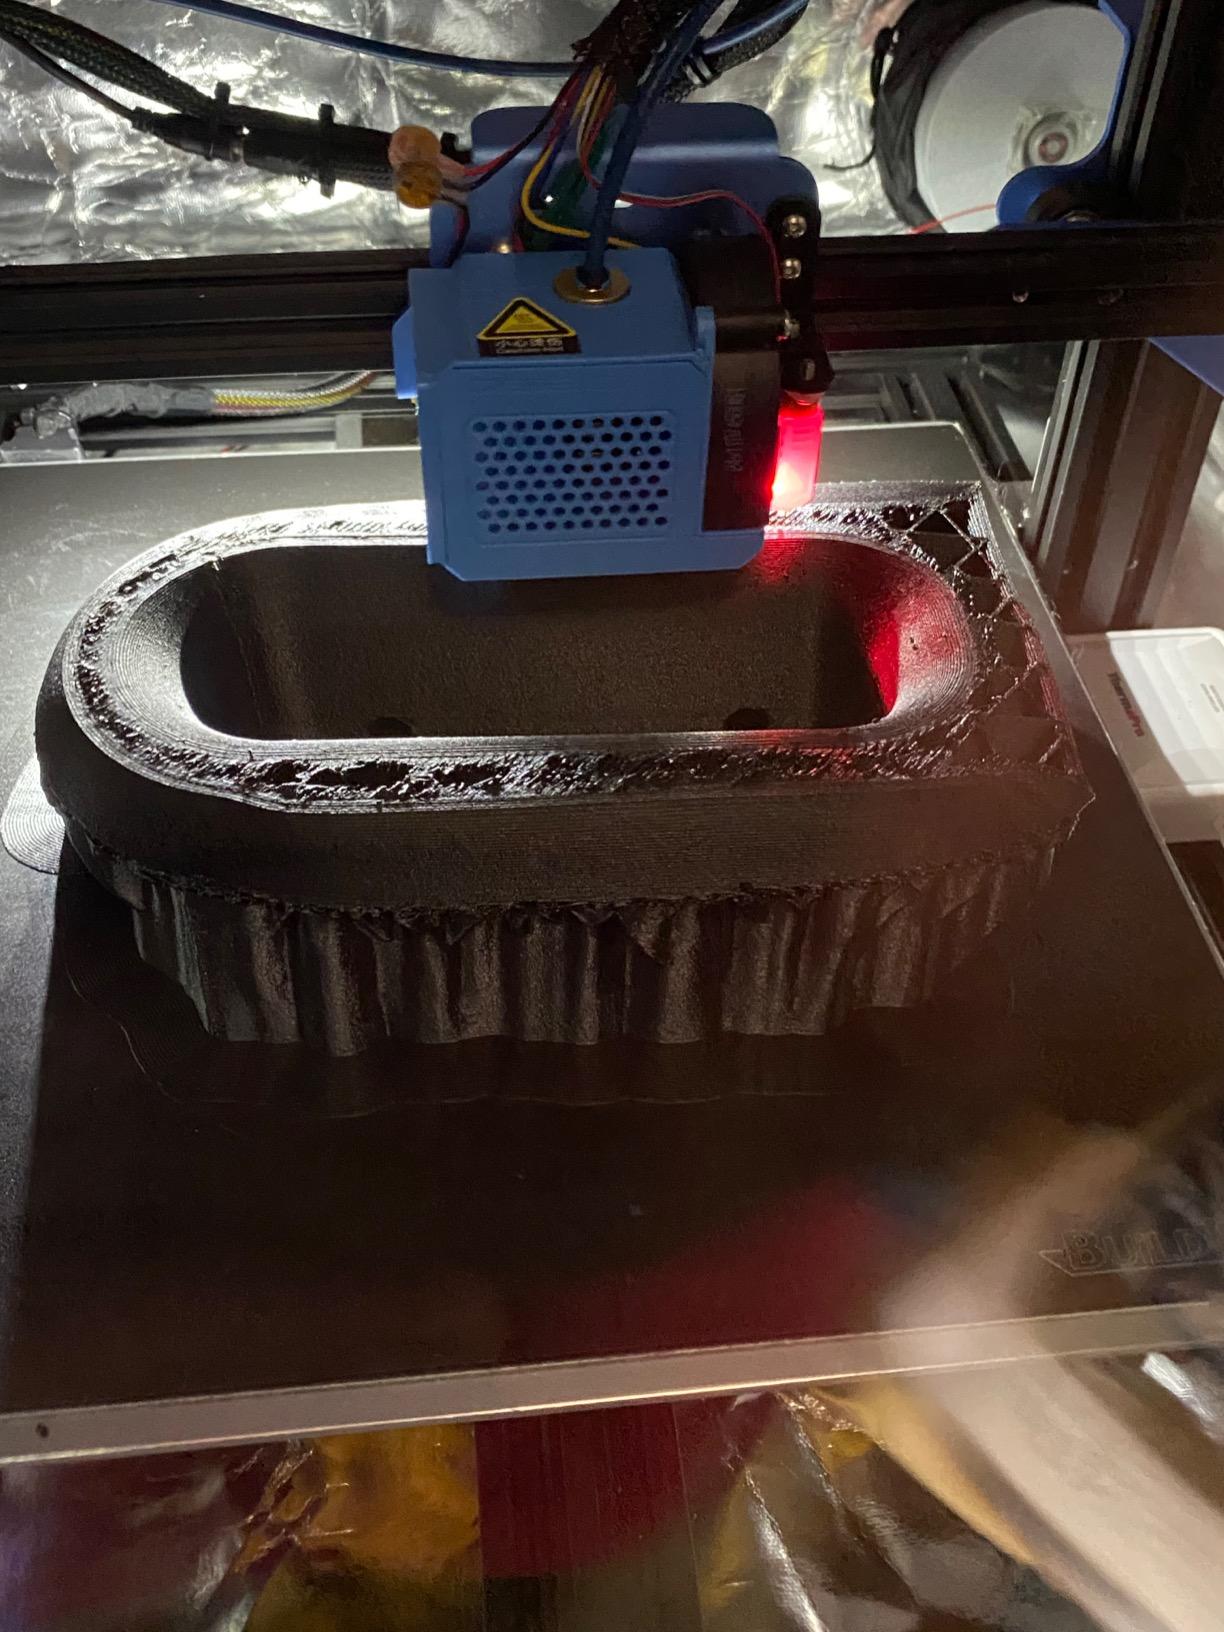
Moisture is a real factor because PC absorbs water readily enough to affect the print, and the manufacturer recommends drying 4-6 hours at 65C before a print. Spools are shipped thoroughly dried, which helps, but a home filament dryer is still worth owning if you buy this regularly.
Two practical notes. A hardened steel nozzle is required, and 0.6 mm or larger is recommended, which is a better choice for a heavily filled abrasive material anyway. Low odor and low VOC output during printing is a genuine plus for a bedroom or office printer, and the matte black industrial finish needs almost no cleanup.
Who this filament suits
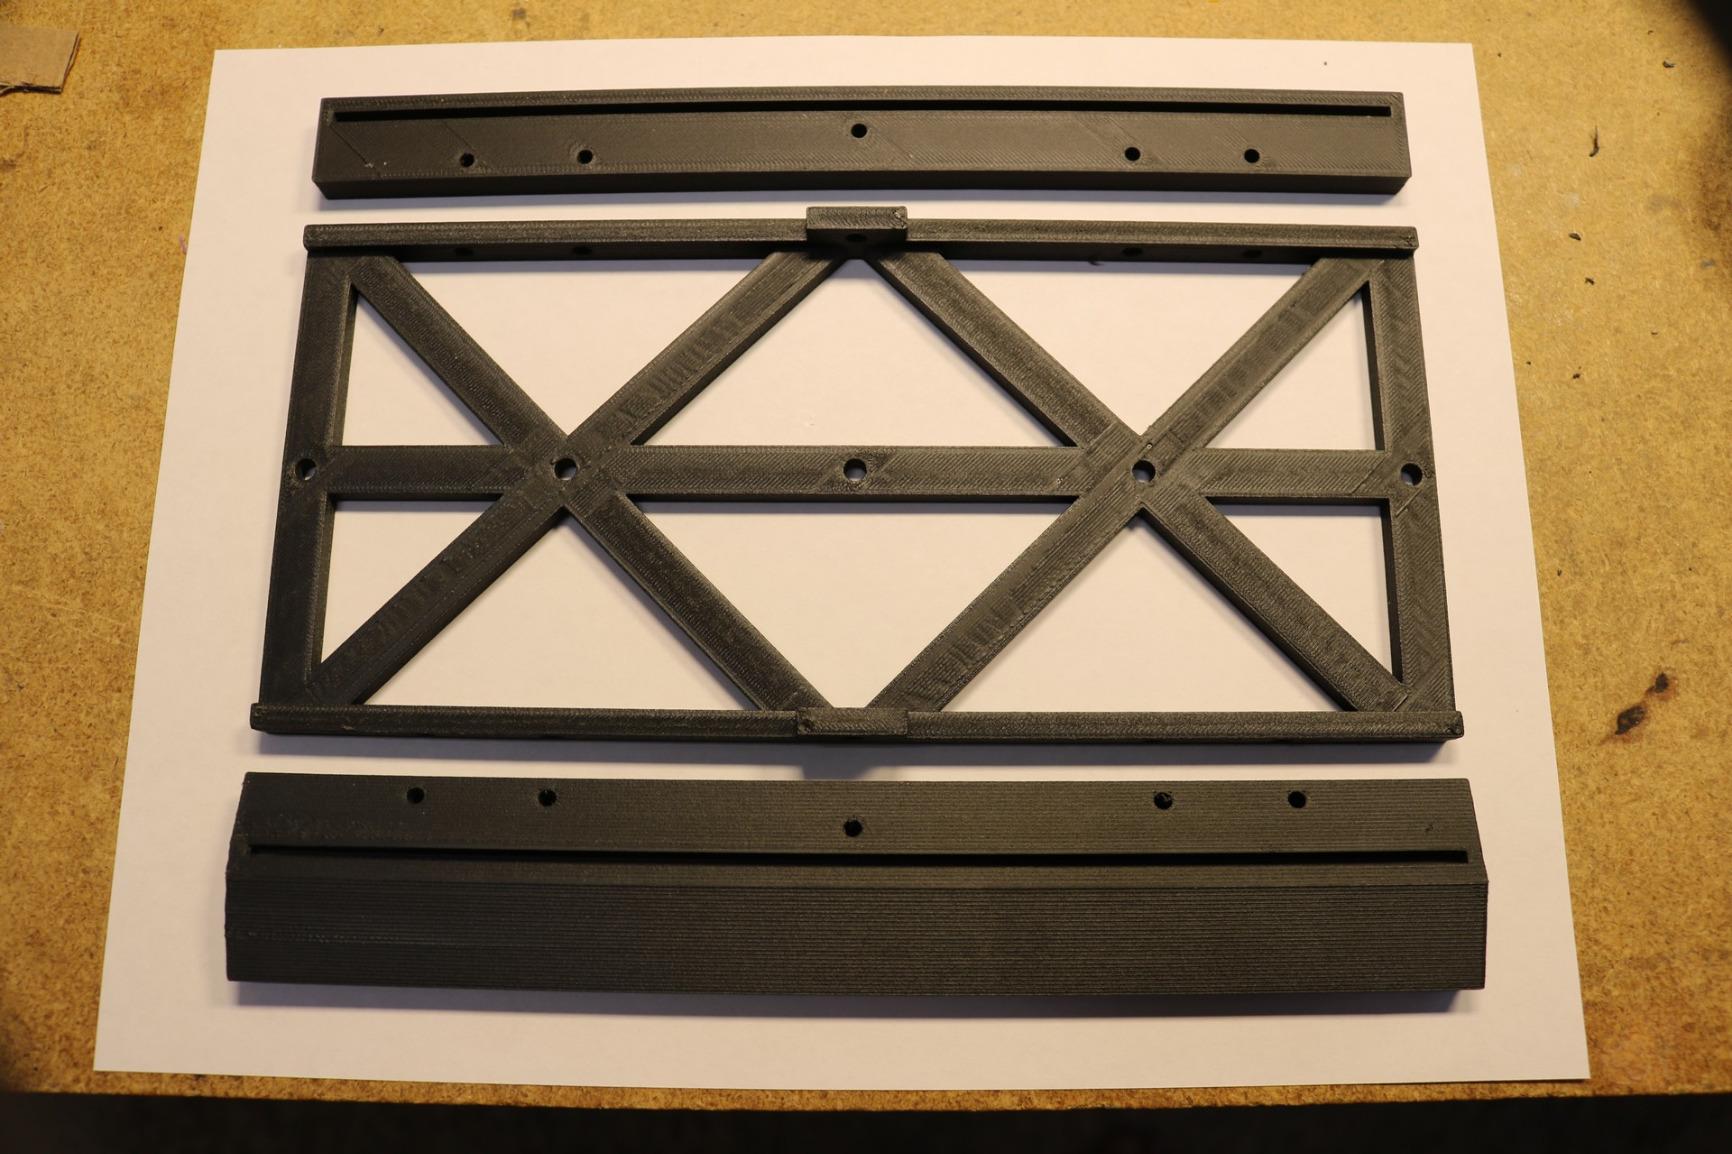
It suits people building heat-exposed hardware: automotive interior brackets, tool handles, jigs and anything that has to survive a workshop without deforming. If you need threaded features in a printed part, the combination of rigidity and thread retention is hard to match with a nylon spool.
It is also a good pick if odor is a genuine problem, since the low VOC output is a real difference from unfilled PC. Expect to spend time tuning the first spool and then keep the profile.
Where it falls short
Several buyers report that the actual resin behaves more like a PC/PLA alloy than full polycarbonate, with lower heat deflection than the name suggests. If you are designing around a specific temperature ceiling, verify the performance yourself rather than trusting the label.
It is also abrasive enough to consume brass nozzles fast, and the spool does not fit standard AMS units well. If you are planning a multi-material setup, this is not the filament for it.
4. SainSmart ePA-CF Carbon Fiber Filled Nylon Filament 1.75mm 1kg
SainSmart 1.75mm Black ePA-CF Carbon Fiber Filled Nylon Filament 1KG (2.2lbs) Spool for 3D Printer
80% nylon with 20% carbon fiber
1.75mm 1kg spool
Nozzle 260-290C
Pros
- Excellent tensile strength and layer adhesion
- Hard and rigid without going brittle
- Good heat and chemical resistance
- Satin industrial finish
- Excellent support release
Cons
- Some reports of nozzle clumping
- Spool-to-spool consistency varies
- Bed adhesion needs glue and a raft
This is the value entry into serious nylon carbon fiber, and it punches well above its position in the list. Reviewers describe it as among the strongest materials they have printed, with a stiffness-to-weight ratio that feels closer to a machined component than to filament. The satin finish reads as an industrial part straight off the printer.
What separates it from a generic reinforced nylon is the toughness. Hard and rigid without being brittle is the phrase that comes up repeatedly, and that is the property that separates a usable mechanical part from a shelf ornament. If your design has thin sections that take a shock, this is a safer bet than a PLA-based alternative.
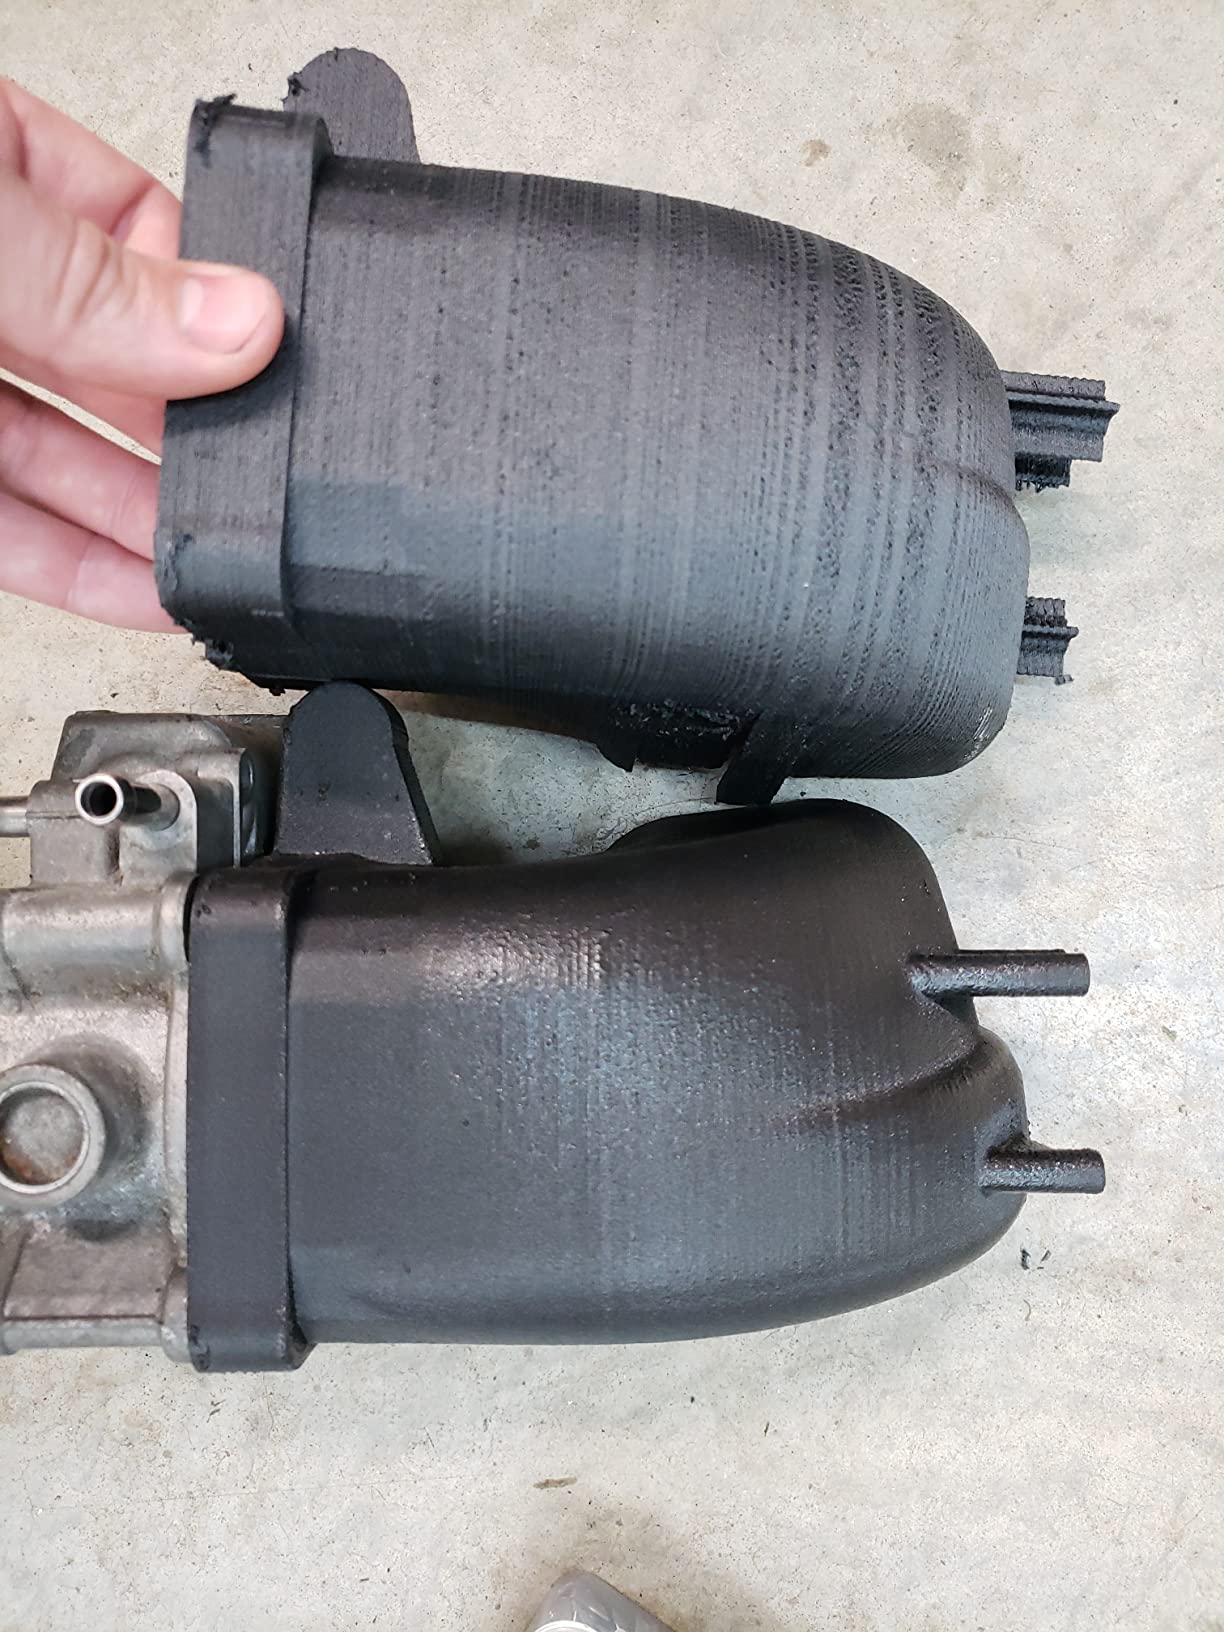
Support release is another genuine plus. Complex geometry on a functional part usually means supports, and material that releases cleanly means less surface work afterwards. The claimed application list covers industrial parts, prosthetics and medical equipment, which tells you what the material is actually tuned for.
Print temperatures sit at 260-290C with a build surface between 45-80C, and the lower shrink rate compared with unfilled nylon reduces the warping that usually makes big nylon parts a problem. An enclosed printer is recommended for layer adhesion, and a stainless steel or hardened alloy nozzle is not optional.
Who this filament suits
It suits makers who want real load-bearing nylon behaviour without stepping up to a premium engineering spool, and it is a strong fit for brackets, mounts and RC components. The high stiffness-to-weight ratio also makes it interesting for anything where grams matter.
If you are moving from PETG-CF and want a big jump in stiffness and heat resistance without losing all impact tolerance, this is the natural step up. The temperature increase is real, so check your hot end can reach it.
Where it falls short
Chopped fiber clumps causing nozzle clogs are the most common complaint, and a few buyers report unusable rolls. Quality consistency between spools is the thing to watch, so inspect the filament before a long print rather than after.
Bed adhesion can require a glue stick plus a raft, and retraction-heavy tuning is often needed to control stringing. Sanding produces hazardous dust and finished parts can irritate skin, so wear a mask and gloves through post-processing.
5. TINMORRY PETG-CF Carbon Fiber PETG Filament 1.75mm 1kg
TINMORRY PETG-CF Carbon Fiber PETG Filament 1.75mm, 1 KG, Black
PETG with 15% short-cut carbon fiber
1.75mm 1kg spool
Nozzle 240-270C
Pros
- Prints easily with almost no warping
- Handles speeds up to 300 mm/s
- Good Z-axis layer adhesion
- Formula reduces clumping and clogging
Cons
- Must be dried at 65C for 8 hours
- Needs a wear-resistant steel nozzle
- Higher infill helps Z adhesion
If your machine is a high-speed Bambu, Creality K1C, QIDI MAX3 or similar, this is the filament designed for it. The manufacturer rates it for speeds up to 300 mm/s, which is unusual for a fiber-filled material and is the reason it earns its place here. Reviewers report strong torsional, tensile and impact behaviour on drone parts and functional models at those speeds.
Warping is close to a non-issue, which cannot be said for most reinforced nylons. The 15 percent short-cut carbon fiber masterbatch is professionally processed, and buyers specifically call out fewer clogs and clumps than traditional PETG-CF, which is the usual complaint about this material class.
Z-axis layer adhesion is described as very good, and for a reinforced PETG that is the headline metric. PETG is normally weak between layers, and the fiber fill plus a well-tuned profile closes much of that gap. Turning the cooling fan off for the first 3 layers is the recommended starting point for bonding.
Settings are 240-270C on the nozzle with a 75-90C bed. Drying is specified at 65C for 8 hours, and the container should be kept below 20 percent relative humidity afterwards, which matters if you are printing over more than one session.
Who this filament suits
It suits owners of fast enclosed printers who want functional CF parts without the tuning marathon that nylon demands. Drone frames, RC components and anything where you print several copies in one session are exactly where the speed rating pays off.
It is also the sensible middle ground for someone who has outgrown PLA-CF but does not have a dryer-heavy nylon workflow yet. The temperature increase over PLA is modest and the enclosure requirement is not absolute for a well-set machine.
Where it falls short
Drying is not optional. Skipping it produces surface roughness and stringing even though the material is more forgiving than nylon. A steel nozzle of 0.4 mm or larger is required, with 0.6 mm better for long runs.
And for genuinely load-bearing work, PETG-CF sits a tier below the nylons and PC blends on stiffness and heat resistance. If the part will be heated, stressed or safety-relevant, go up a family rather than tuning harder here.
6. SUNLU PA6-CF20 Carbon Fiber Nylon Filament 1.75mm 1kg
SUNLU PA6-CF20 Carbon Fiber Nylon 3D Printing Filament 1.75mm, 1KG, Black
80% PA6 with 20% carbon fiber
1.75mm 1kg spool
Nozzle 270-290C
Pros
- Strong layer adhesion
- Very little warping on long parts
- PA6 withstands up to 209C
- Vacuum packed and dry from the box
Cons
- Must be dried before printing
- Not compatible with AMS units
- Rough surface at 20 percent fiber
This is the affordable route into 20 percent loaded PA6, and reviewers consistently compare its performance favourably against premium PA6-CF brands on a cost-per-kilogram basis. The heat figure is the standout: the manufacturer states PA6 here withstands up to 209C, and users report prints that survived hot embers without softening.
Warping is remarkably low, including on long 320 mm parts printed without a brim, which is a meaningful result for a nylon. That dimensional stability is what makes it a good fit for large flat components where shrinkage would normally ruin the design.
Annealing is the step most people skip and the one that makes this material interesting for strong parts. The recommendation is 80-130C for 5-12 hours, which raises the heat performance of the finished part and stabilises its dimensions. Accuracy is quoted at +/- 0.03 mm on a standard 203.2 mm spool.
The spool ships vacuum packed with desiccant, and users report losing very little weight during the first drying cycle, which is a useful signal about factory conditioning. Recommended settings are a 270-290C nozzle, 50-70C bed and a deliberately slow 50-150 mm/s print speed.
Who this filament suits
It suits builders of large mechanical parts, fixtures and heat-exposed components who want a genuine 20 percent fiber load without the premium tier price. Gears, fan blades, chassis parts and bicycle components are all within its stated range.
If you plan to anneal finished parts to raise their heat rating, this is one of the few affordable spools where the manufacturer publishes an annealing schedule. That makes it useful for anyone building fixtures that see workshop temperatures.
Where it falls short
It is not compatible with AMS or AMS Lite multi-color systems because the fiber-filled filament is too brittle for the feeder path. The recommended workaround is to bypass the extruder gear and use a feed assist, which is one more thing to set up.
Blobs and zits appear quickly if you print it wet, and the 20 percent load leaves a rough surface texture. A loose winding on some spools has also caused tangling and filament snaps, so check the spool when it arrives.
7. Polymaker Fiberon PA612-CF15 Carbon Fiber Nylon Filament 1.75mm
Polymaker Fiberon PA612-CF15 Carbon Fiber Nylon Filament 1.75mm, Black, 0.5kg
15% carbon fiber in PA612 nylon
0.5kg spool
HDT 175C after annealing
Pros
- Published tensile and HDT figures
- Lower moisture pickup than PA6
- Easy to print for an engineering nylon
- Stiff without becoming brittle
Cons
- Wears through AMS gears without the bypass
- 0.5kg spool is small
- Abrasive on unhardened nozzles
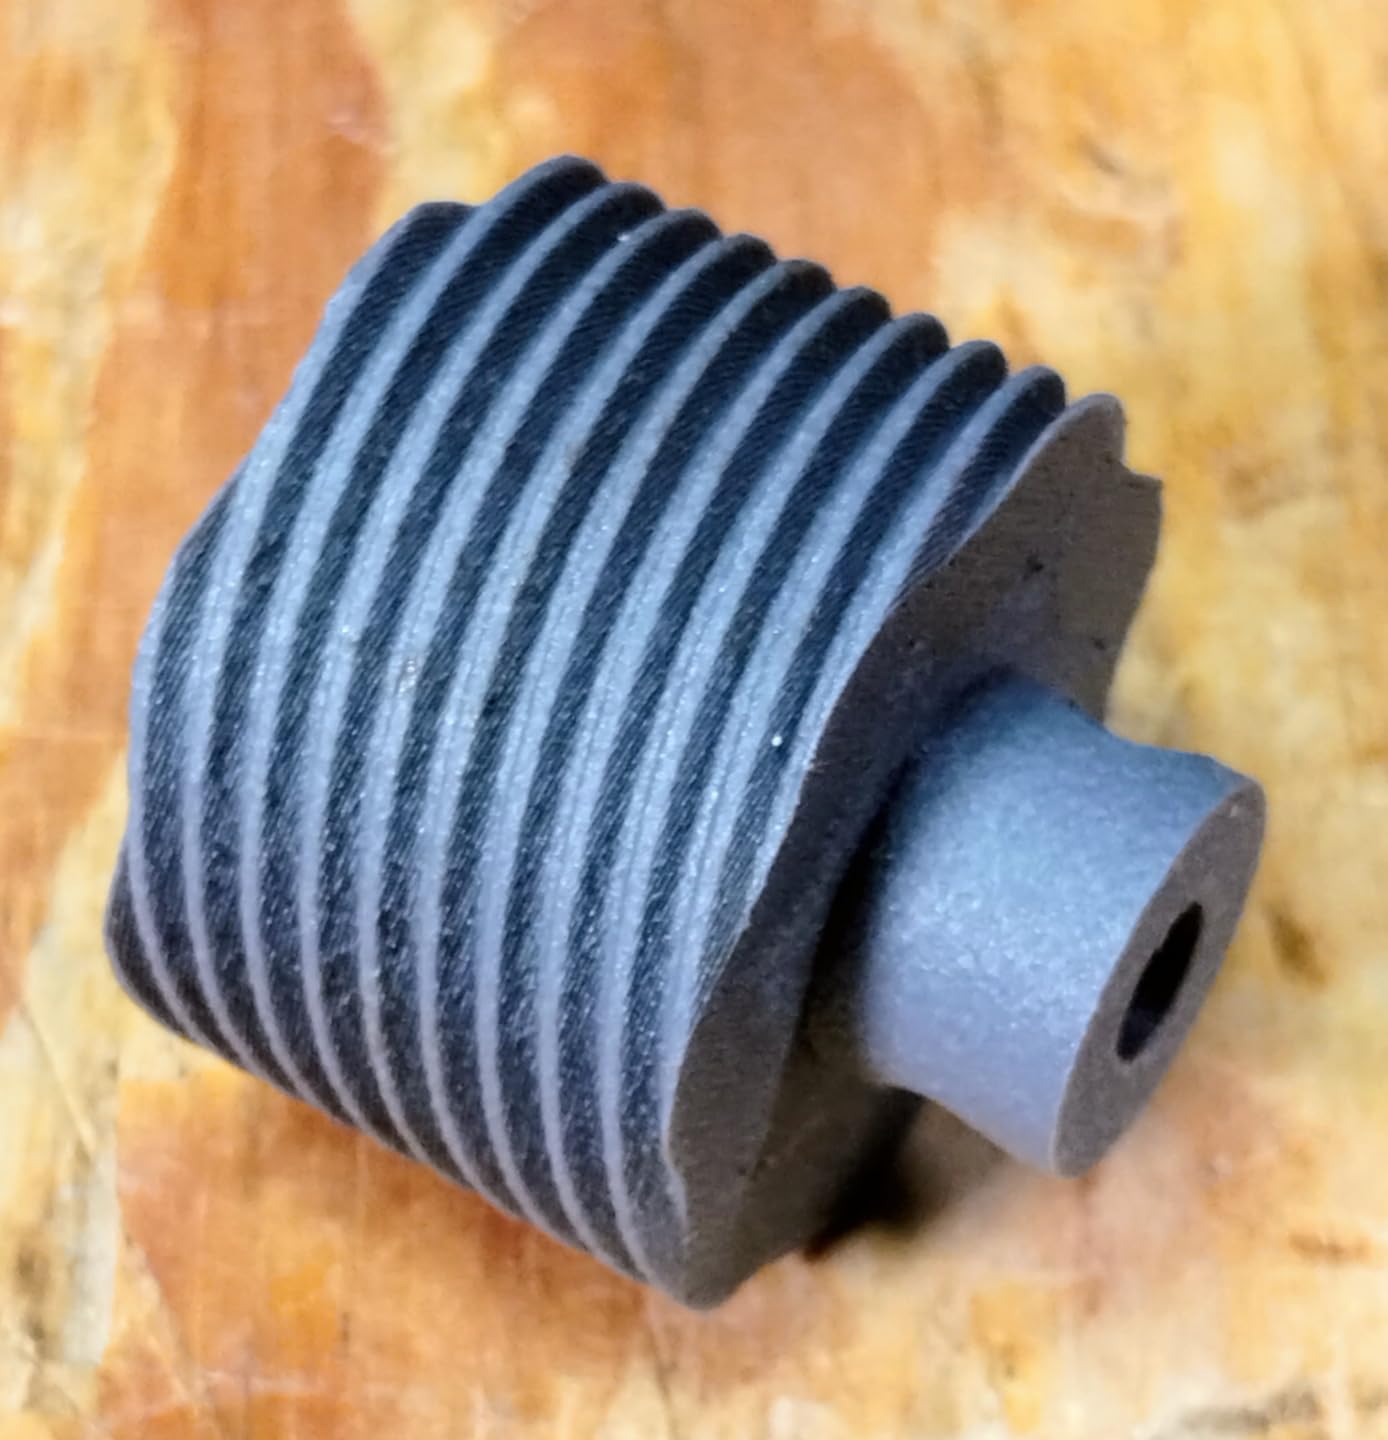
This is the only spool in the roundup with a full published strength data sheet, and that alone puts it ahead for anyone who has to justify a material choice. Polymaker quotes 91.9 MPa dry X-Y tensile strength, 83.1 MPa after annealing and moisture conditioning, and a heat deflection temperature of 175C at 0.45 MPa after annealing at 100C for 16 hours. Very few competitors publish numbers you can actually check.
The base is long-chain PA612 rather than PA6, which is the whole point for damp environments. It takes on noticeably less water than PA6, so parts keep their dimensions and their stiffness in humid conditions instead of softening and swelling. For a garage, a workshop or anything outdoors in variable weather, that is a real functional advantage.
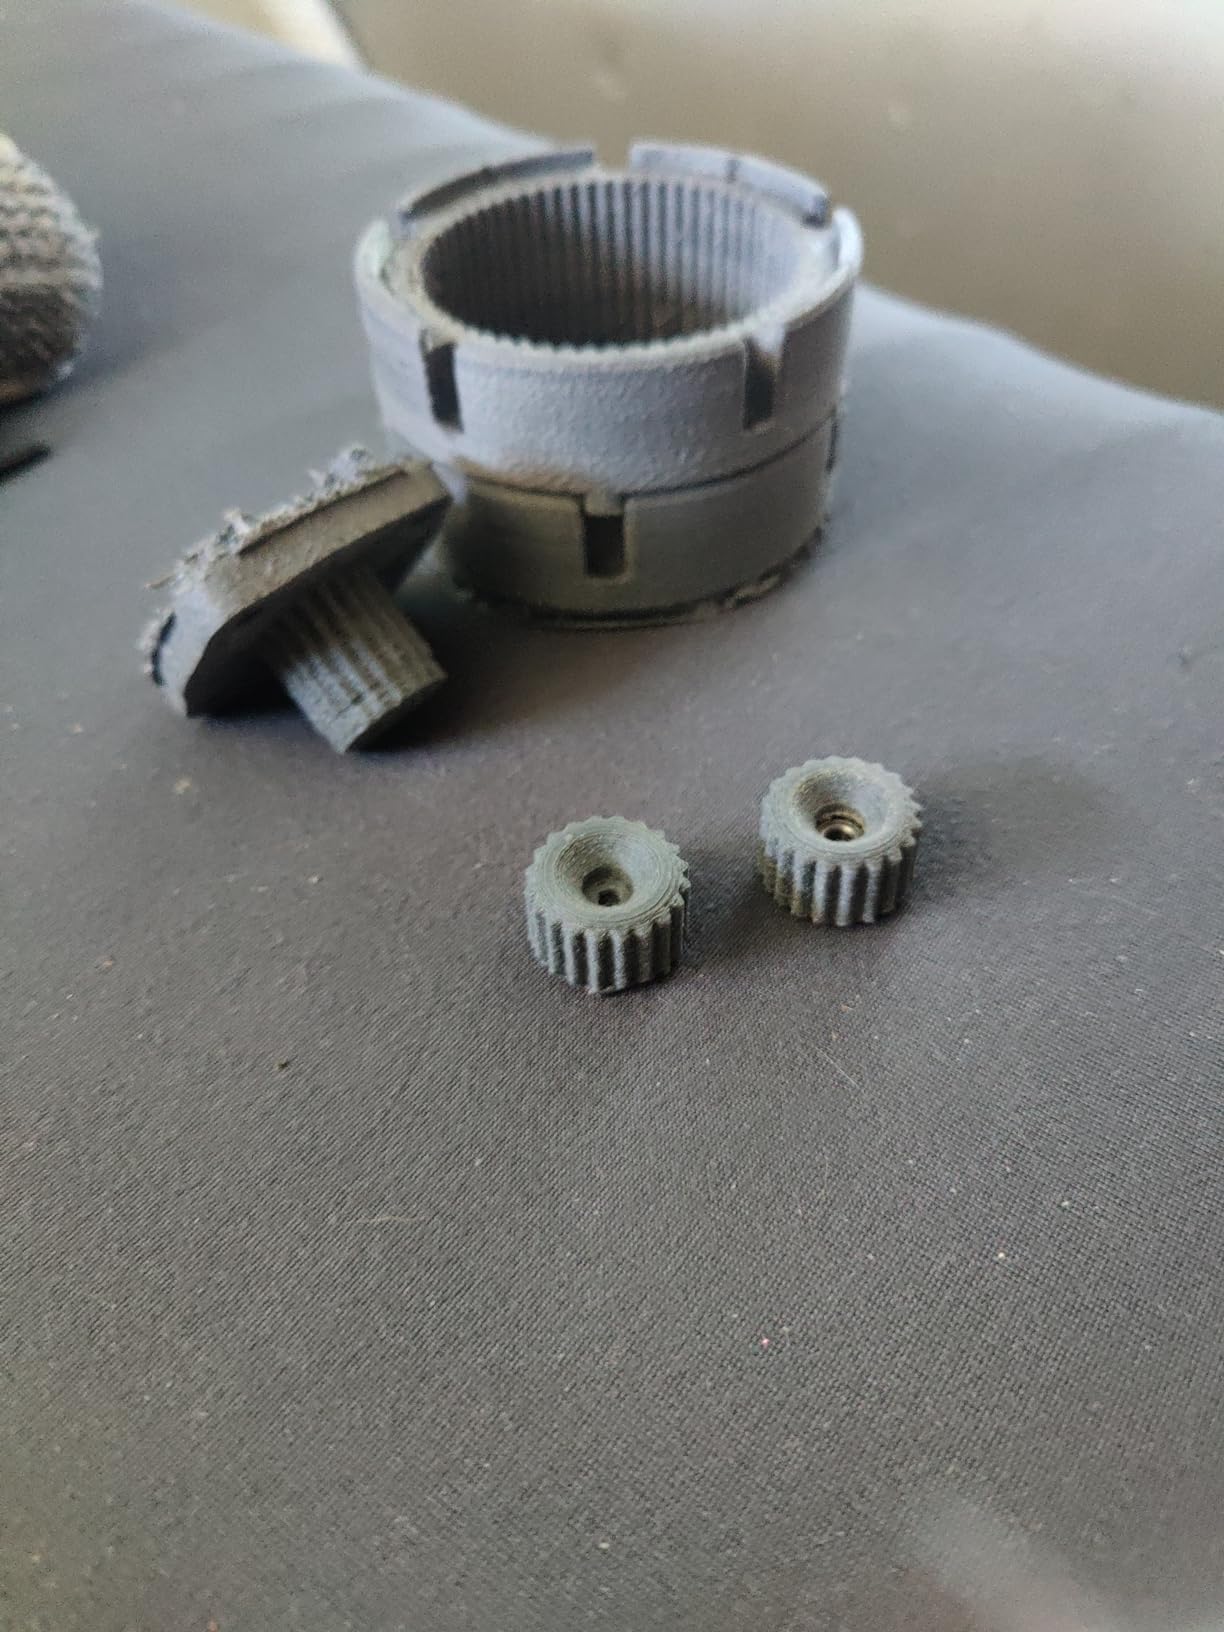
Despite the engineering pedigree, reviewers describe it as easy to print, almost like PLA, with a clean matte black finish. Minimal warping for a nylon is reported even on open-frame machines, and the parts come out stiff without the brittleness that usually accompanies high fiber loads.
The requirements are an all-metal hotend, a 250-300C nozzle, a 40-50C build plate, a hardened steel or ruby nozzle and the fan off. Drying at 100C for 10 hours is specified if the filament has been exposed to humidity, and storage below 20 percent relative humidity is recommended even for this low-absorption nylon.
Who this filament suits
It suits anyone who works in a humid space, prints parts that will live outdoors, or simply wants the strongest documentation in the category. The published tensile and HDT numbers let you design against real limits instead of guessing from a product name.
It also suits people who want engineering performance without an enclosure-heavy workflow. The low warping means open-frame printers are viable, and the wide temperature window gives room to tune.
Where it falls short
The 0.5 kg spool is small and expensive relative to larger formats, so you will replace it often. If you print heavily, budget for the restock rather than the single spool.
It is stiff enough to grind through AMS and AMS HT extruder gears unless you fit the bypass and a TPU feed assist. Printing above 300 mm/s also degrades surface quality noticeably, even though the material can run at those speeds. And like every spool here with real fiber content, it will wear an unhardened nozzle quickly.
8. Polymaker Carbon Fiber PLA Filament Black 1.75mm 1kg
Polymaker Carbon Fiber PLA Filament Black 1.75mm 1KG, Strong & Rigidity
Carbon fiber reinforced matte PLA
1.75mm 1kg spool
Nozzle 190-230C
Pros
- Carries a 4.7 average from buyers
- Very easy to print with smooth extrusion
- Neat winding reduces tangles
- Accuracy at +/- 0.02 mm
Cons
- Must be dried before printing
- Brass nozzles wear faster
- Low heat resistance overall
This one carries a 4.7 average with 85 percent of reviews at the top star. What that rating reflects is consistency rather than extreme capability: smooth extrusion, a tough matte finish, and a spool wound neatly enough that feeding interruptions are rare. For a part that has to look finished straight off the bed, it is the most reliable result in our tests of the PLA-based options.
Stiffness is a clear upgrade over standard PLA, which is where most of the reinforcement benefit lands for this kind of part. The dimensional accuracy is quoted at +/- 0.02 mm with a 1.75 mm tolerance compatible with most desktop FDM printers, so it drops into an existing setup without hardware changes.
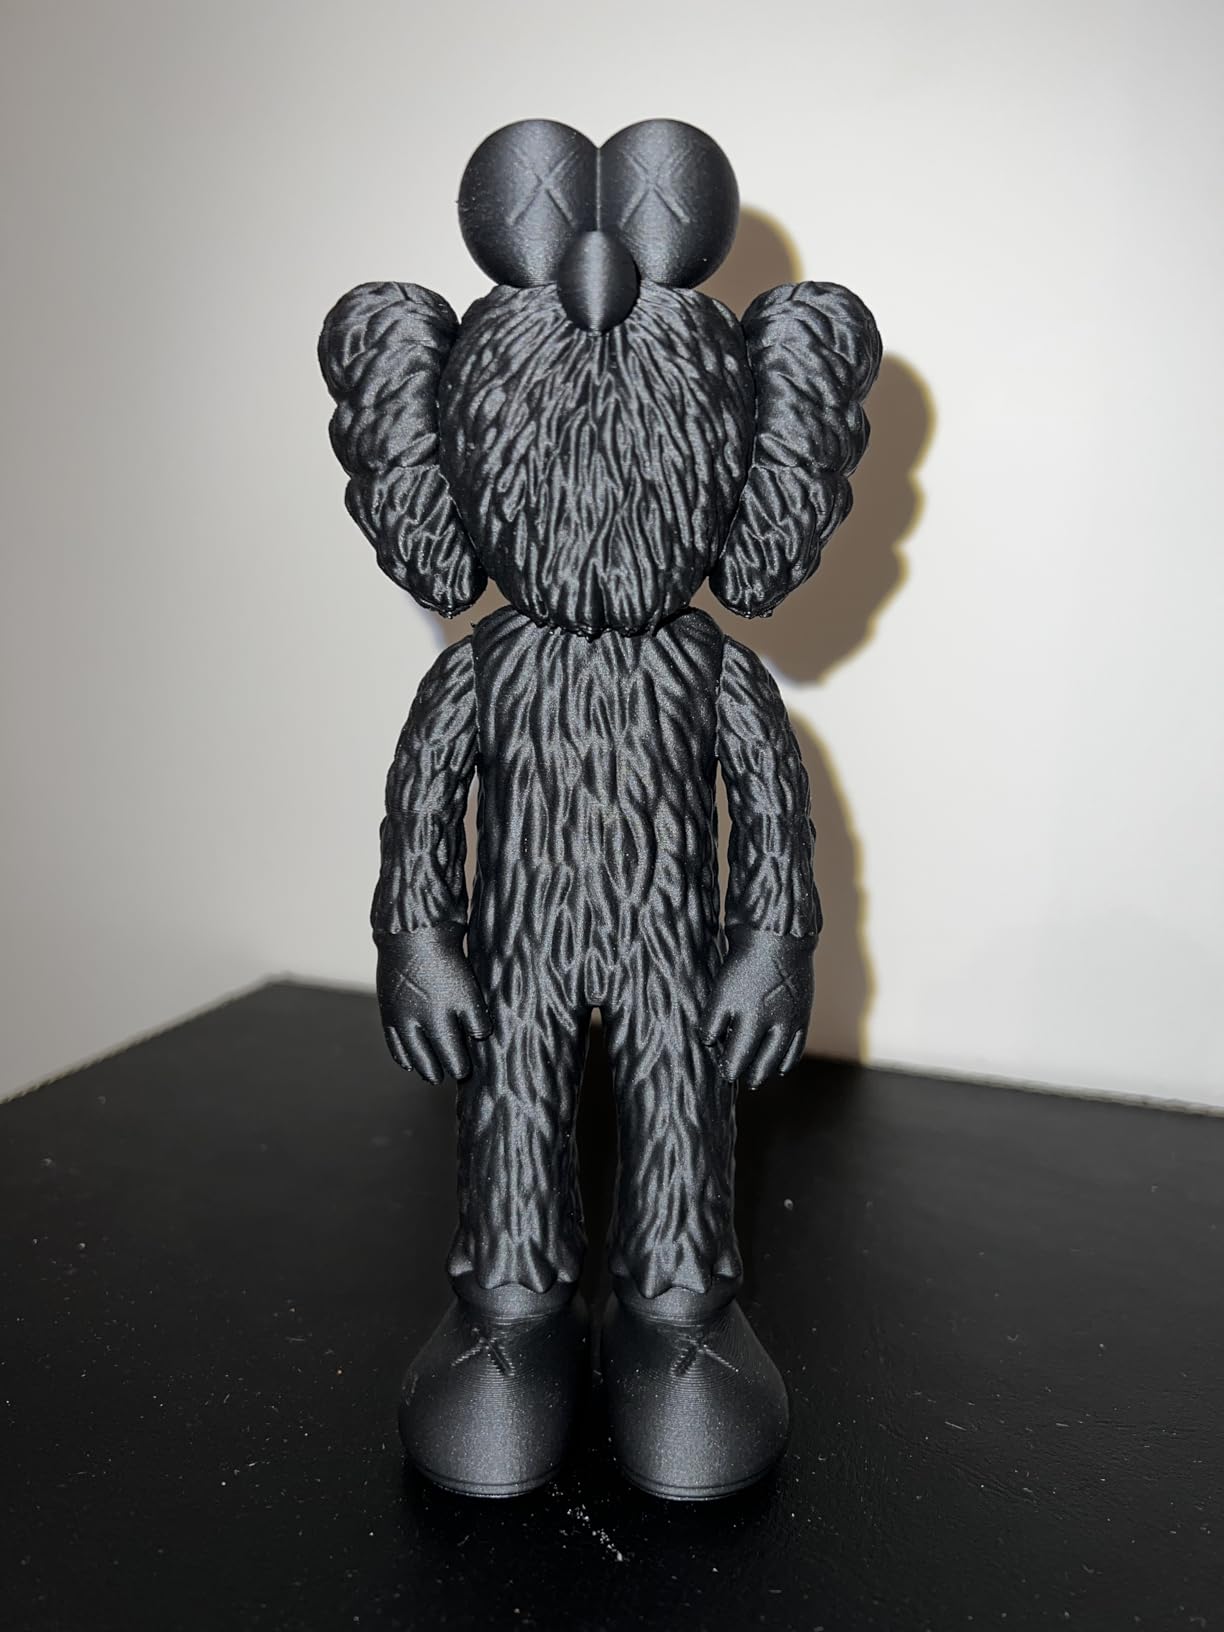
Recommended printing speed is 100-200 mm/s with a 190-230C nozzle, and a bed temperature between 25-60C. That is an ordinary PLA temperature window, so an entry-level printer with a brass nozzle and no enclosure can run it, which is unusual for a carbon fiber filament.
The recycled cardboard spool and moisture-proof packaging are sensible touches, and the color is a deep matte black rather than a grey that looks like unfinished filament. For visible parts, that finish does more for the result than any post-processing step.
Who this filament suits
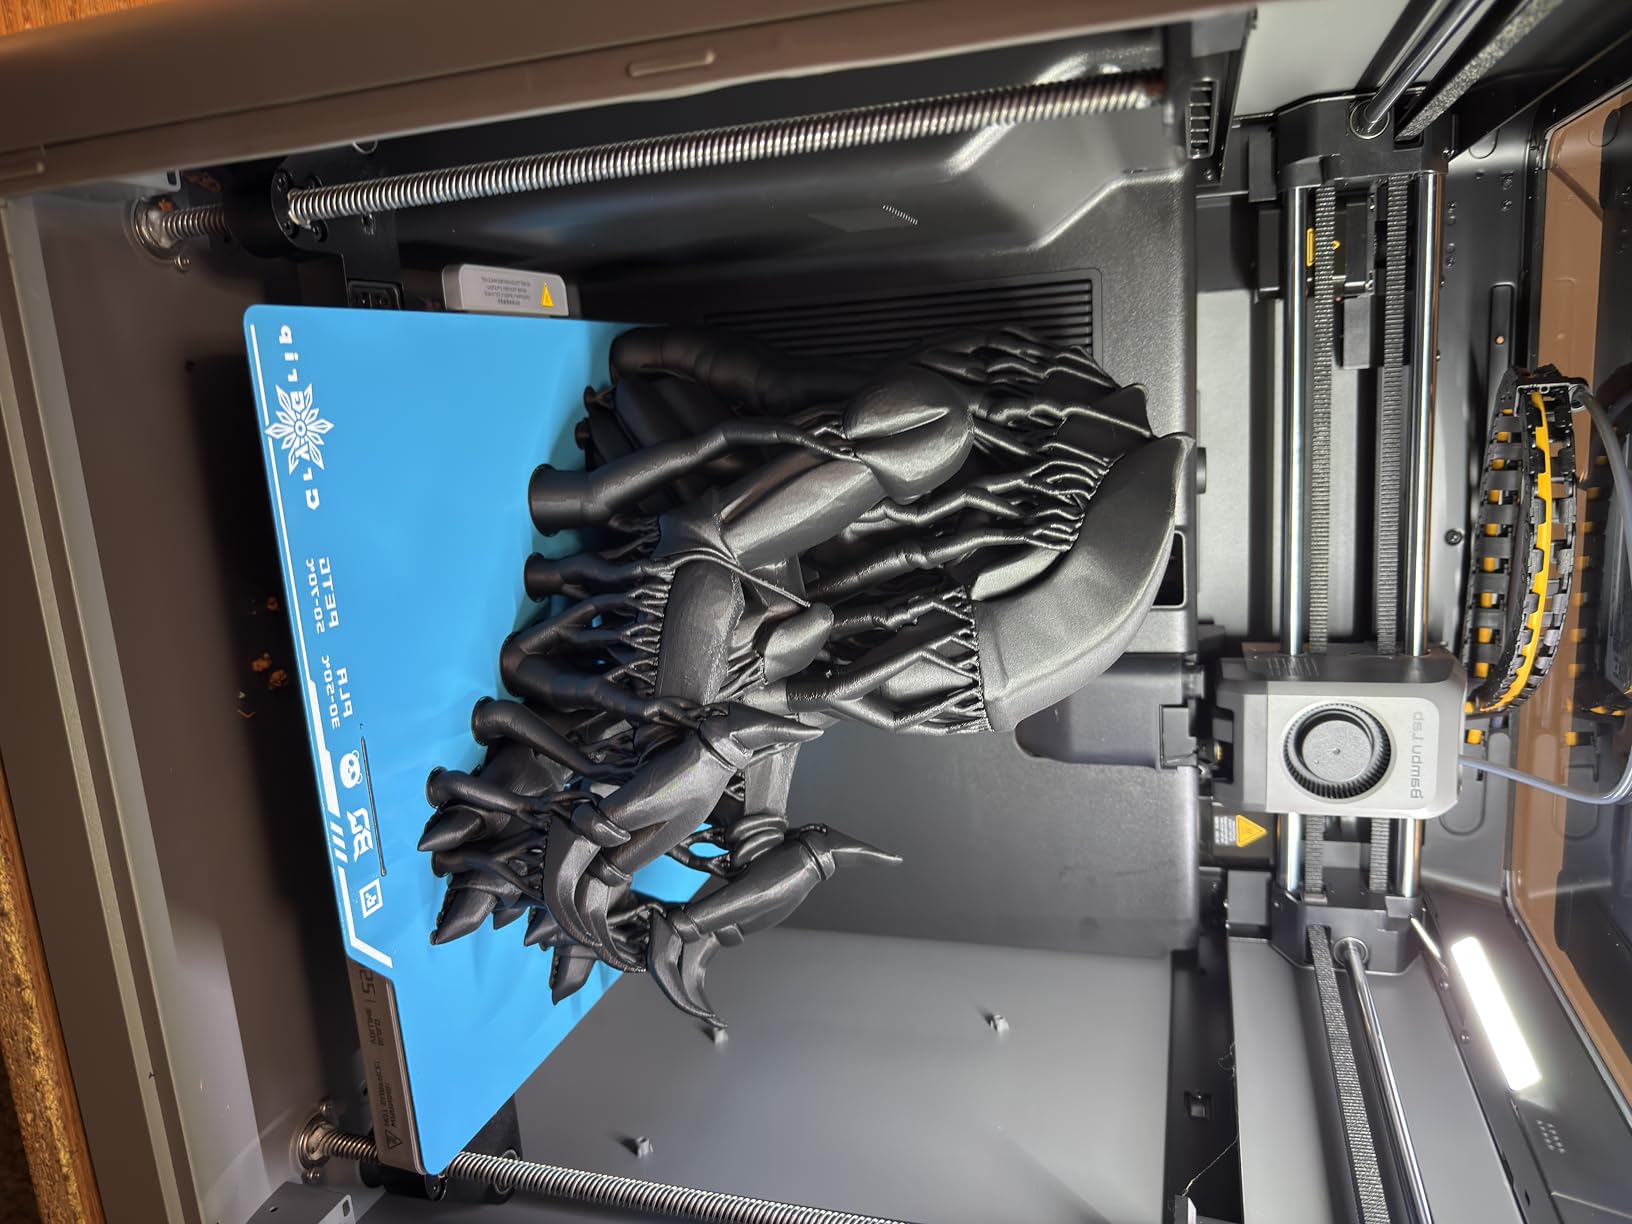
It suits anyone who wants a visibly finished, rigid part with the minimum possible hardware investment. Camera mounts, drone shrouds, display models, desk hardware and cosplay pieces all benefit from the combination of matte finish and rigidity.
If you are building a camera rig or a mount that needs to stay rigid on a tripod head, our carbon fiber tripod roundup covers the same stiffness-versus-weight thinking in a different form factor.
Where it falls short
Its heat resistance is well below that of the nylon and PC blends, and that gap matters. Do not put a printed part from this spool in a hot car, near an engine, or anywhere the temperature climbs.
It is still abrasive, so brass nozzles wear faster even at PLA temperatures. The reinforced matrix is also more brittle than plain PLA, which matters if the design relies on flexing rather than holding shape. For a part that has to bend and survive, pick a reinforced PETG instead.
9. ELEGOO PETG-CF 3D Printer Filament 1.75mm Black 1KG
ELEGOO PETG-CF 3D Printer Filament 1.75mm Black 1KG
PETG with carbon fiber
1.75mm 1kg spool
Nozzle 240-270C
Pros
- Tough with strong impact resistance
- Abrasion resistant for gears and bearings
- Fine matte texture hides layer lines
- Reliable extrusion with little stringing
Cons
- Can clog at very fine layers
- Cardboard spool is weak
- Print corners can lift
This is the best value pick and carries a 4.7 average with 84 percent five-star reviews. What separates it from cheaper PETG-CF is toughness. Reviewers specifically call out high impact resistance and less tendency to fracture under stress, which is the weakness that limits most fiber-reinforced PETG.
Abrasion resistance and dimensional accuracy are the other standouts, and the intended applications are gears, bearings and structural parts. Those are sliding and rotating contacts, where a part that is merely stiff will wear and a part that is stiff and dimensionally stable will run.
Extrusion is reported as reliable with little to no stringing, even after only partial drying, which is a genuine convenience compared with nylon-based options. The fine matte texture reduces visible layer lines without the slightly shiny look some reinforced PETG finishes develop under direct lighting.
Settings are 240-270C on the nozzle with a 65-75C hotbed, and compatibility is described as universal for common 1.75 mm FDM printers. A hardened steel nozzle no smaller than 0.4 mm is the stated requirement, and the spool is wound well enough to work in CFS and AMS-style units.
Who this filament suits
It suits anyone who wants functional strength without committing to nylon temperatures, drying discipline and an enclosure. Moving up from plain PETG is a small change and the impact resistance jump is real, which is why this is a common first step for functional parts.
It is also a sensible pairing with flexible filaments on a two-spool machine, since a rigid bracket printed alongside a TPU grip solves a problem no single material handles. Our TPU filament guide covers the flexible half of that combination.
Where it falls short
Fine layers are the weak point. At or below 0.12 mm layer height, clogging can occur, so keep the layer height at a normal value and resist the urge to print decorative thin-wall parts with this spool.
Print corners can lift slightly, which is a design consideration as much as a settings one. The cardboard spool is also weak for AMS use without a printed adapter, and the finish can read as slightly shiny under some lighting.
10. SUNLU PA12-CF 20% Carbon Fiber Nylon Filament 1.75mm 1KG
SUNLU PA12-CF 20% Carbon Fiber Nylon 1.75mm 3D Printing Filament, Black 1KG
80% PA12 with 20% carbon fiber
1.75mm 1kg spool
Heat resistance to 175C
Pros
- PA12 absorbs less water than other nylons
- Resists grease gasoline and solvents
- Low density at 1.04 g/cm3
- Spool rated for 110C drying
Cons
- Must be dried before printing
- Not for AMS or multi-color systems
- Needs a hardened steel nozzle
PA12 is the least water-absorbing nylon family, and that single property drives everything else about this spool. Parts resist swelling and humidity, so a part printed today and used outdoors next month keeps its fit. If your work touches grease, gasoline or solvents, the chemical resistance is the reason to choose it over a PA6-based alternative.
Density is listed at 1.04 g per cubic centimetre, which the manufacturer frames as metal-like strength at low weight. The stated applications are bike helmets, drone frames and car parts, and that combination of low mass and high heat resistance is genuinely hard to get elsewhere on a desktop printer.
Heat resistance is rated up to 175C, which sits between the PA6-CF20 spool and the premium PA612 option. The surface is described as low friction and wear resistant, so it suits gears, bearings and sliding mechanisms where a higher-friction nylon would eventually wear in and jam.
Recommended settings are a 260-280C nozzle, a 50-70C bed and a 60-150 mm/s speed. Drying is specified at 80C for 12 hours or 110C for 4 hours, and the supplied spool is a heat-resistant design rated to 110C so it can go straight into a dryer.
Who this filament suits
It suits anyone printing parts for outdoor, automotive or workshop use where moisture and chemical exposure are the main risks. Drone frames and lightweight helmets benefit from the low density, and anything that sees heat benefits from the 175C ceiling.
It is also the spool to reach for when a nylon part has to stay dimensionally stable across seasons rather than just survive a single print. That is a slow-burning benefit, but it is the one that prevents a returned part.
Where it falls short
It has the smallest review base in the group at 98 ratings, so the long-term consistency picture is less established than the PA6 options. The 4.4 average is solid, but there is less evidence of spool-to-spool reliability.
Drying is required before printing or you get stringing and a rough surface, multi-color systems are not recommended because the filament breaks in feeders, and copper nozzles wear quickly. Glue or a similar bed adhesive helps with edge warping on larger parts.
Why the Base Polymer Matters More Than the Carbon Fiber Label
The carbon fiber label tells you what reinforces a filament, not what the filament is made from. A reinforced PLA and a reinforced PA6 share almost nothing except surface finish, and that is the whole reason the picks above are ordered by polymer family rather than by brand.
Here is the honest framing for anyone comparing families. PLA-CF gives you stiffness and rigidity at low temperature with almost no hardware requirements, and it is the least tough option in the group. PETG-CF adds genuine impact resistance and easier printing than any nylon, at the cost of top-end stiffness and heat resistance. Nylon-based CF, whether PA6, PA612 or PA12, is the load-bearing tier with far better toughness than its stiffness figures suggest. PC-CF sits alongside nylon for heat and dimensional performance. PPA-CF would sit above all of them, but no spool in this roundup carries it.
Manufacturer test methods differ, and that caveat belongs next to any number you read. Heat deflection temperature is usually quoted at 0.45 MPa and only the PA612 spool here states the pressure and the annealing condition it was measured under, which is the difference between a comparable figure and an advertising one.
There is also a consistency signal worth using. Spools that publish fiber content, dimensional tolerance and either HDT or tensile data are telling you something a matte black finish cannot. The spools here that state their 15 or 20 percent fiber load are the ones worth trusting for structural work.
Print Settings and Drying by Filament Family
Reinforced filament punishes guessed settings more than plain material does, because the fiber changes the melt behaviour and because the abrasive content destroys brass hardware. The families cluster tightly enough that you can learn one profile and adjust, rather than calibrating ten separate spools.
For PLA-CF, run a 190-230C nozzle, a 25-60C bed and 100-200 mm/s. Dry only if the spool has been open. For PETG-CF, use 240-270C with a 65-90C bed, keep the fan off for the first 3 layers, and dry at 65C for 8 hours before the first print and whenever the spool has been exposed. Dry filament that prints fine but rough, since roughness is the earliest warning sign of absorbed moisture.
For nylon-based CF, the pattern is 260-290C with a 50-80C bed, the fan off, and speeds between 50 and 150 mm/s. Drying is the part people skip and regret: the PA6 options specify 80C for 12 hours or 110C for 4 hours, and the PA612 option specifies 100C for 10 hours. If your dryer cannot hold 100C, use the longer 80C schedule rather than shortening the hotter one.
For PC-CF, expect 255-280C, a 90-100C bed, fan fully off, and a dry of 4-6 hours at 65C. Speed matters more than most settings here because layer adhesion is fragile at high print rates on PC. And across every family, print a small coupon before committing filament to a long functional job, because a delaminated part discovered at hour 20 is the expensive outcome.
The Real Strength Levers: Walls, Infill, Layer Height and Orientation
If a carbon fiber part snapped, the filament is not always the culprit. Four settings change the strength of a printed part more than the choice between two spools of the same material, and none of them are hard to adjust.
Walls matter more than infill. A part with three or four perimeters holds far more load than the same part at 100 percent cubic infill with two walls, because the load path runs through the wall thickness and the perimeters bond to every layer. Set walls first. Infill is what stops a part flexing; it is not what stops it breaking.
Layer height is the quiet one. Fiber-filled material needs a minimum layer height of roughly 0.2 to 0.25 mm to bond properly, and thin layers on reinforced filament are a common cause of delamination. Below that, fibers are not fully encapsulated and the layers pull apart.
Orientation is a strength decision, not a finishing decision. The Z axis is the weakest direction in any FDM print, so a bracket that carries load should be printed so that the load runs through the X-Y plane, not across the layer bonds. Rotating a part ninety degrees in the slicer is often the single biggest strength improvement available. If you want a flexible or impact-resistant part, the same logic says do not use reinforced PLA at all.
Carbon Fiber vs Glass Fiber: Which Reinforcement to Buy
Glass fiber reinforced filament is the cheaper alternative and it is not a bad one. The trade-off is simple: carbon fiber is stiffer, lighter and darker with a better matte finish, while glass fiber is heavier, cheaper per kilogram and slightly tougher in some formulations.
Choose carbon fiber when stiffness-to-weight matters, when the part will be seen, or when heat and stiffness together are the requirement. Choose glass fiber when the budget is the constraint on a large print, when the part is hidden, or when you want reinforcement without the cost. Both are abrasive and both need a hardened nozzle, so the hardware requirement does not change.
How to Tell If a Spool Is Short on Fiber
Short-stuffed fiber is a genuine community complaint, and it is fair to be sceptical of any spool that refuses to state a percentage. The check is simple: if the listing does not name the fiber weight percentage, treat it as decorative until proven otherwise.
Beyond the spec sheet, two physical signals tell you something. Underfilled filament usually prints with a noticeably glossier surface, because less exposed fiber means less of that characteristic matte texture. And a properly filled spool should feel and behave predictably at temperature, giving the low shrinkage and stable dimensions that a thin fiber load cannot deliver. Annealing a small printed coupon and watching for dimensional change is the most reliable test you can run at home.
Safety: Handling Ultrafine Carbon Particles at Home
Chopped carbon fiber in filament is bound into the pellet and is not airborne in the way pure fiber dust is, but printing and post-processing still release fine particles. An enclosure with a HEPA or activated carbon filter is the single most effective upgrade for anyone printing reinforced filament regularly.
Ventilate the room, and never print reinforced nylon in a closed bedroom without filtration. When you sand, cut or machine a finished part, wear a respirator and gloves and work outdoors or with extraction, because that is where the dust is genuinely hazardous. Clean the printer’s fan and heatsink on a schedule, since the abrasive dust settles there.
Frequently Asked Questions
Which carbon fiber filament is the strongest?
The strongest options here are the engineering-polymer spools rather than the ones with the highest fiber number. For load-bearing parts our picks are the IEMAI PA6-CF with 20 percent chopped fiber in a PA6 nylon base, rated to 150C, and the Polymaker Fiberon PA612-CF15, which publishes 91.9 MPa dry X-Y tensile strength and a 175C heat deflection temperature after annealing. The PLA-CF options are stiff but brittle, and PETG-CF is tough without being the strongest.
Does carbon fiber make filament stronger?
Partly, and not in the way most people assume. Chopped carbon fiber raises stiffness, improves dimensional stability, reduces shrinkage and lightens the part, but it does not add much tensile strength and it usually reduces impact toughness. The base polymer decides the strength ceiling, which is why reinforced PLA can be more brittle than plain PLA while reinforced nylon is dramatically stronger than either.
Is PLA CF as strong as PETG?
No. PETG-CF is stronger in impact and general toughness, and it tolerates more abuse before it cracks, while PLA-CF is stiffer and finishes more attractively. Neither matches a nylon-based or PC-based carbon fiber filament for load-bearing work. If the part takes shock, choose PETG-CF. If it must hold a static load at temperature, step up to nylon or polycarbonate.
What is the ideal print temperature for carbon fiber filament?
It depends on the base polymer rather than the fiber content. PLA-CF prints between 190 and 230C, PETG-CF between 240 and 270C, nylon-based CF between 260 and 290C, and PC-CF between 255 and 280C. Hardened steel nozzles conduct heat less efficiently than brass, so reinforced filament often needs a higher temperature than the unfilled version. Start at the top of the range and work down.
Is it okay to dry PA6-CF filament at 70C?
Yes, and 70C is a reasonable starting point, but published schedules go higher for a reason. The SUNLU PA6-CF20 in this roundup is specified at 80C for 12 hours or 110C for 4 hours, while the Polymaker PA612-CF15 specifies 100C for 10 hours. If your dryer cannot exceed 70C, extend the time rather than shortening it, and always cool the spool sealed before opening it.
Do I need an enclosure for carbon fiber nylon?
For the nylon-based spools, yes. PA6-CF and PA12-CF both list a closed chamber as the condition for best results, because nylon warps badly without chamber control and layer adhesion suffers. The one partial exception is the Polymaker PA612-CF15, which reviewers report printing with minimal warping even on open-frame machines. PETG-CF and PLA-CF do not need an enclosure.
How much infill do I need for strong CF parts?
Infill is less important than most guides suggest. For load-bearing carbon fiber parts, set three or four perimeters first, because the load path runs through the walls. Then use 40 to 60 percent infill as gyroid or cubic for internal structure. Keep layer height at 0.2 mm or above so the fiber is properly encapsulated, and orient the part so the load runs through the X-Y plane rather than across layer bonds.
Final Verdict for Strong Parts in 2026
For most people reading this, the OVERTURE PLA Matte CF is the right first buy. It has the largest review base in the group at 6,824 ratings, it prints on ordinary hardware, and the matte finish means parts look finished without post-processing. Start there if your parts are stiff, not load-bearing.
For genuinely strong parts, choose by base polymer. Nylon-based carbon fiber such as the IEMAI PA6-CF or the SUNLU PA6-CF20 carries static load and heat; the Polymaker Fiberon PA612-CF15 is the pick when the part lives in a damp environment or you need published numbers to design against; the PRILINE PC-CF handles the highest heat. For parts that take shock rather than load, the ELEGOO and TINMORRY PETG-CF spools are hard to argue with.
Whatever you pick, install a hardened nozzle, dry the spool before the first print, print a coupon, and set your walls before your infill. That last habit is the difference between a strong part and a wasted spool. These are the best carbon fiber filaments for strong parts available in 2026, and the right one depends far more on your base polymer and your printer than on the fiber percentage.